Spread across a modern manufacturing infrastructure, Aviva Equipments delivers complete dairy plant sections engineered for hygiene, productivity and reliability.
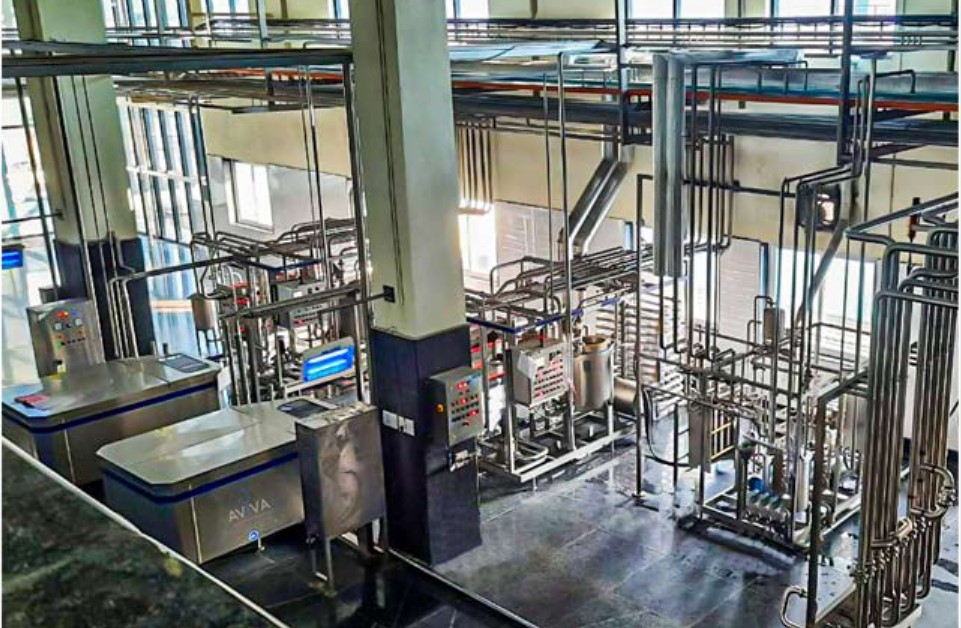
The can reception section in a dairy industry is where raw milk is received, stored, and inspected in hygienic conditions before processing.
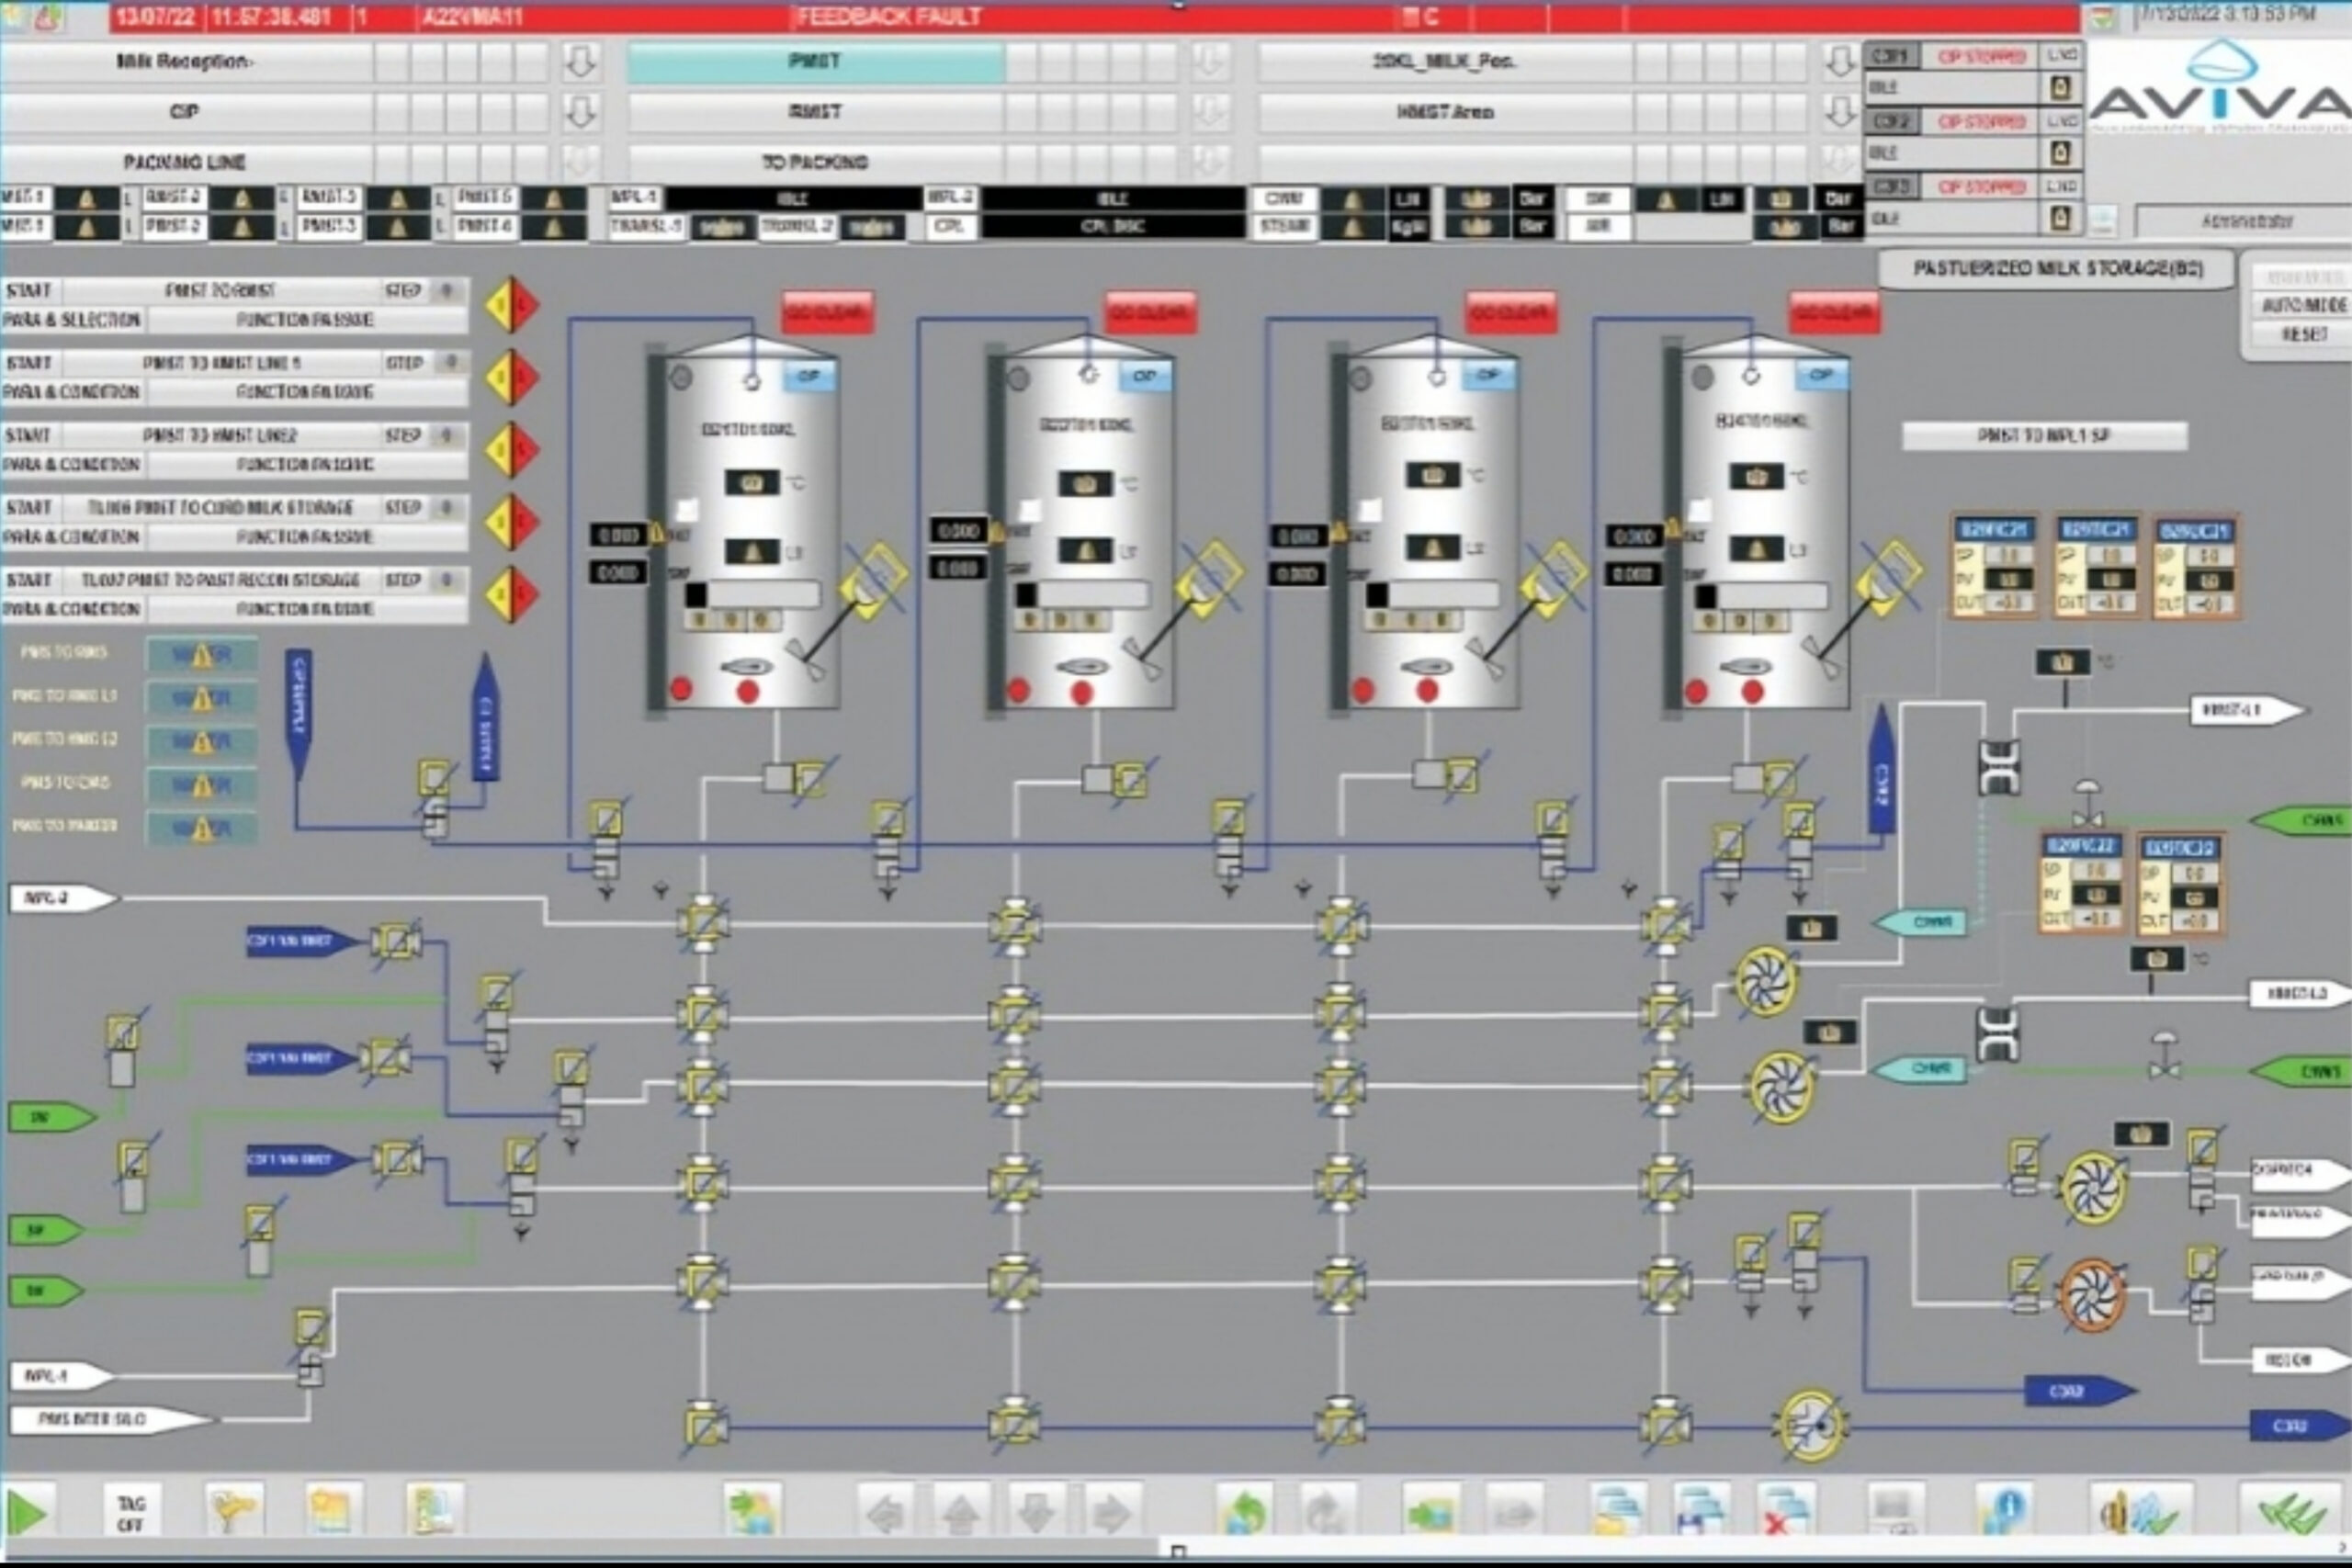
SCADA-based automation refers to the use of Supervisory Control and Data Acquisition (SCADA) systems to monitor and control industrial processes and operations in real-time.
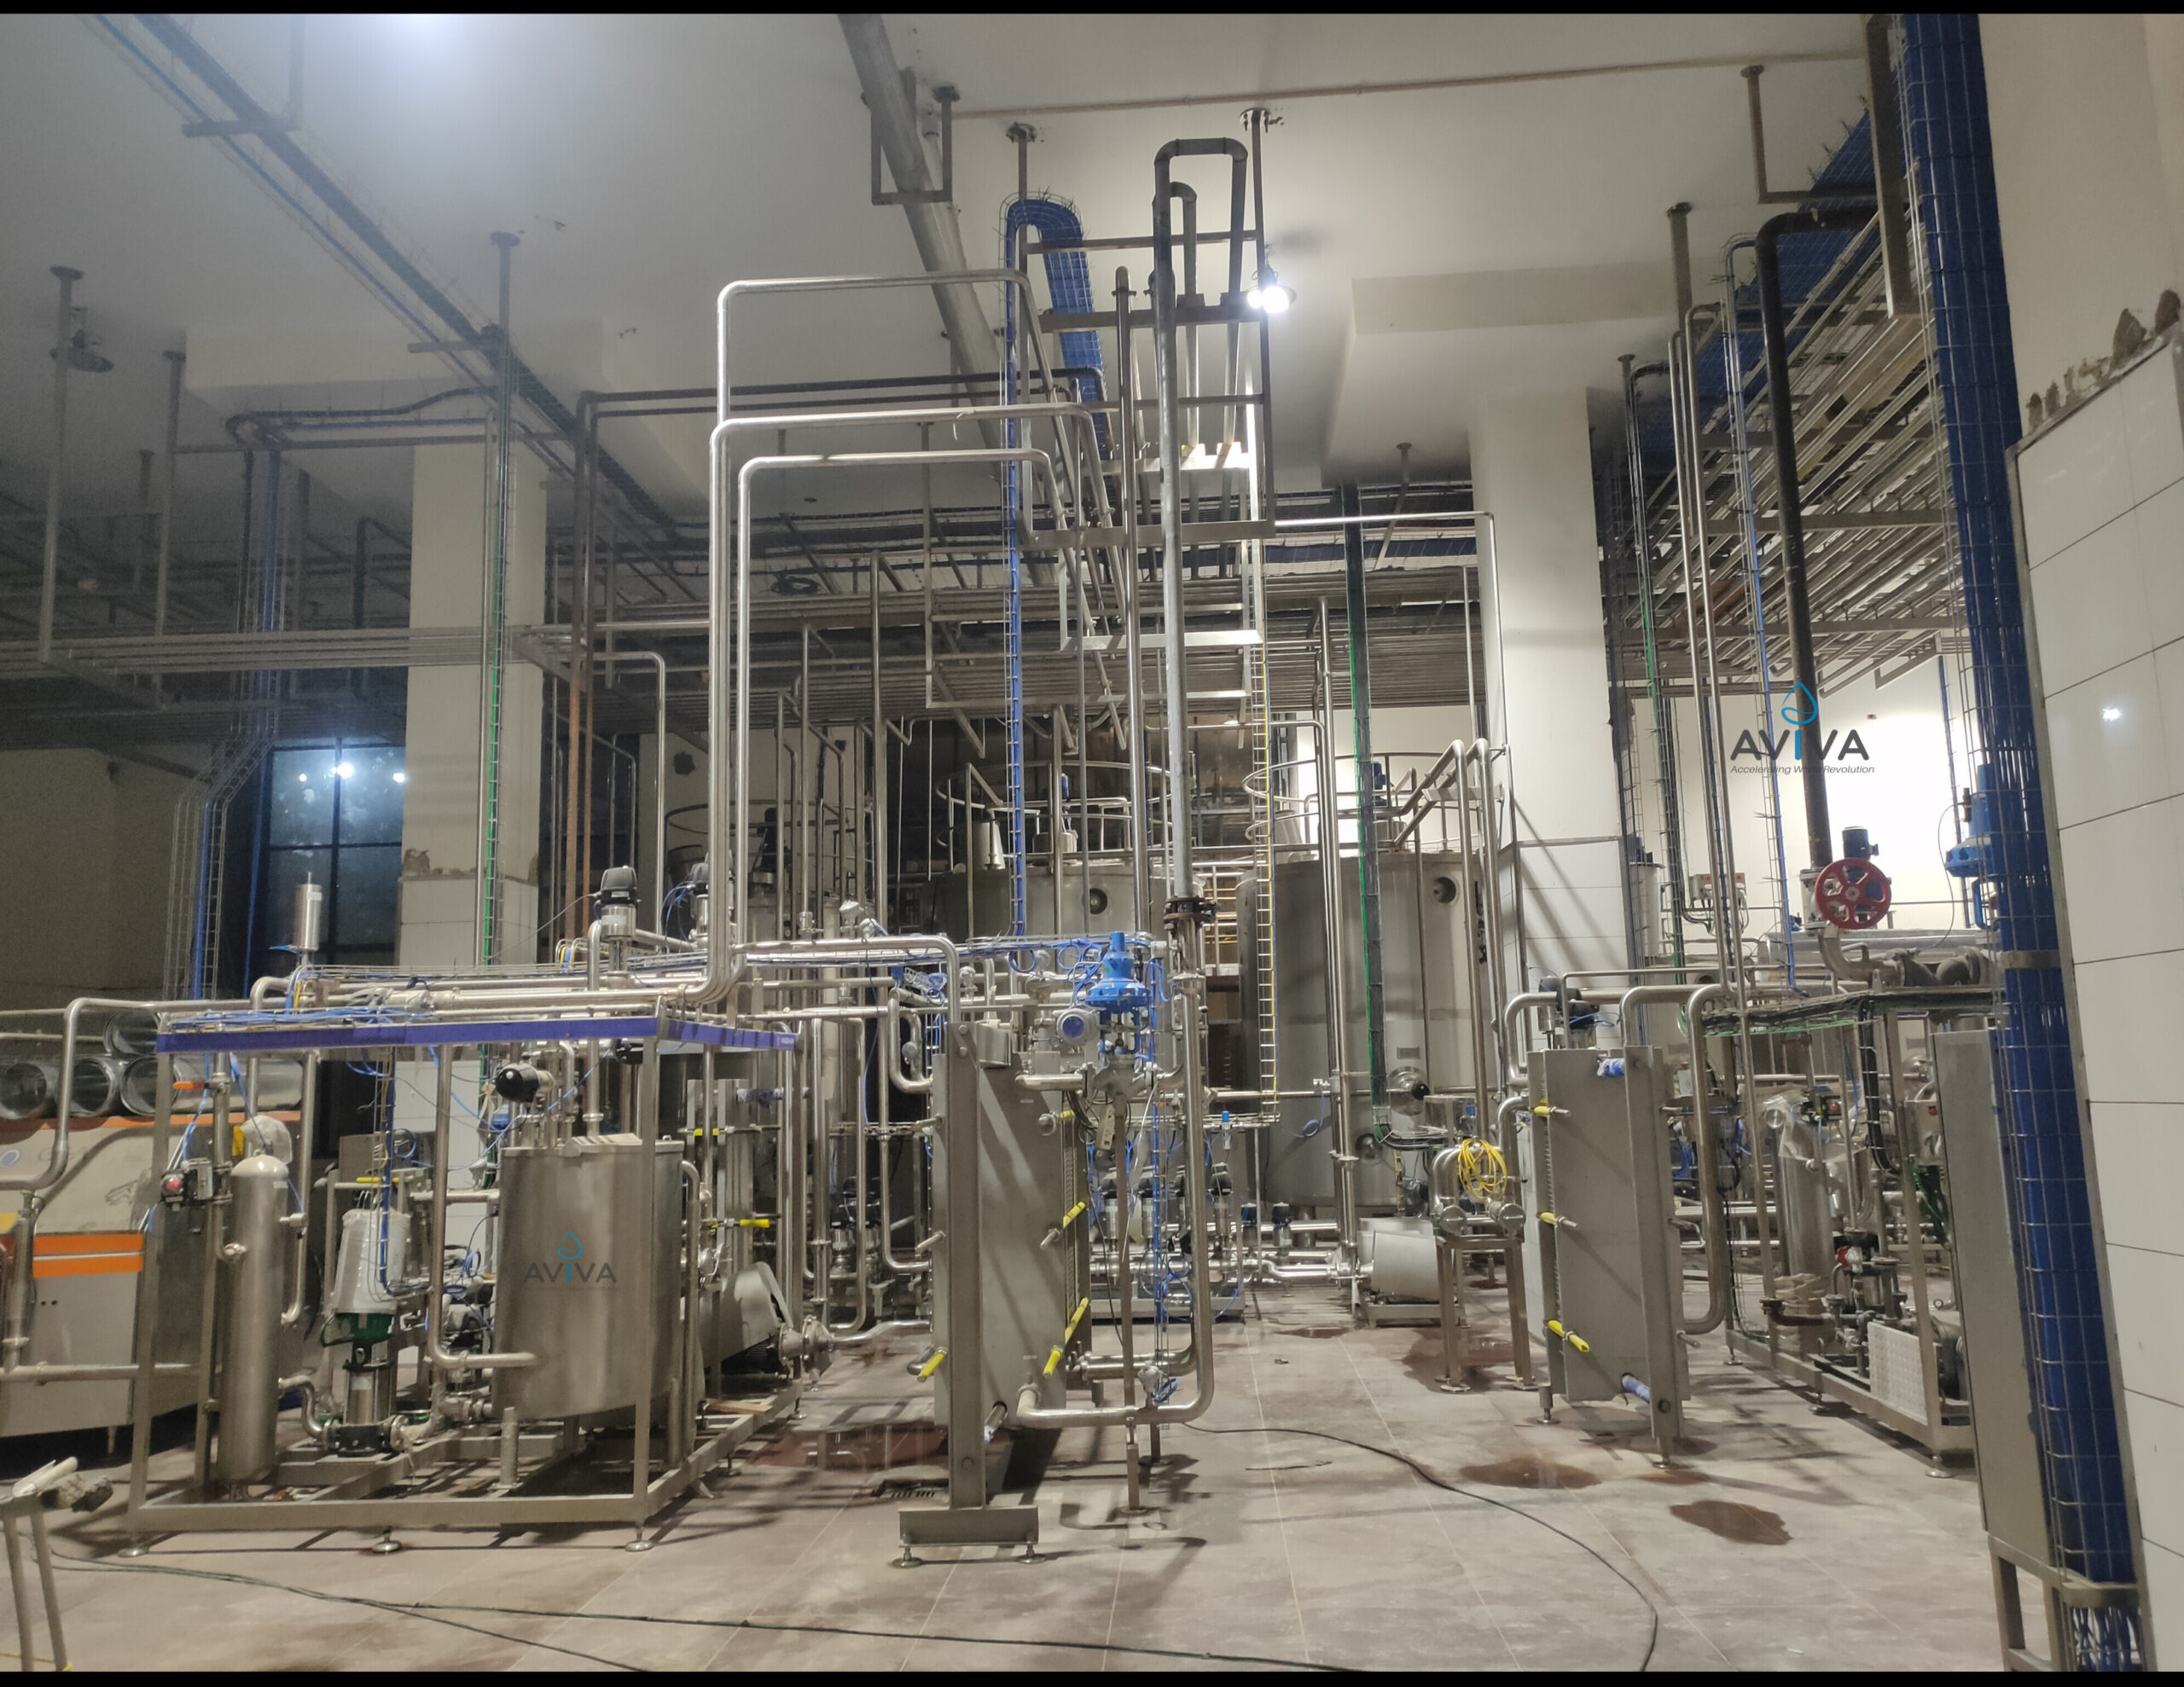
Complete ice cream plant solutions designed and manufactured for hygienic dairy processing with reliable performance.
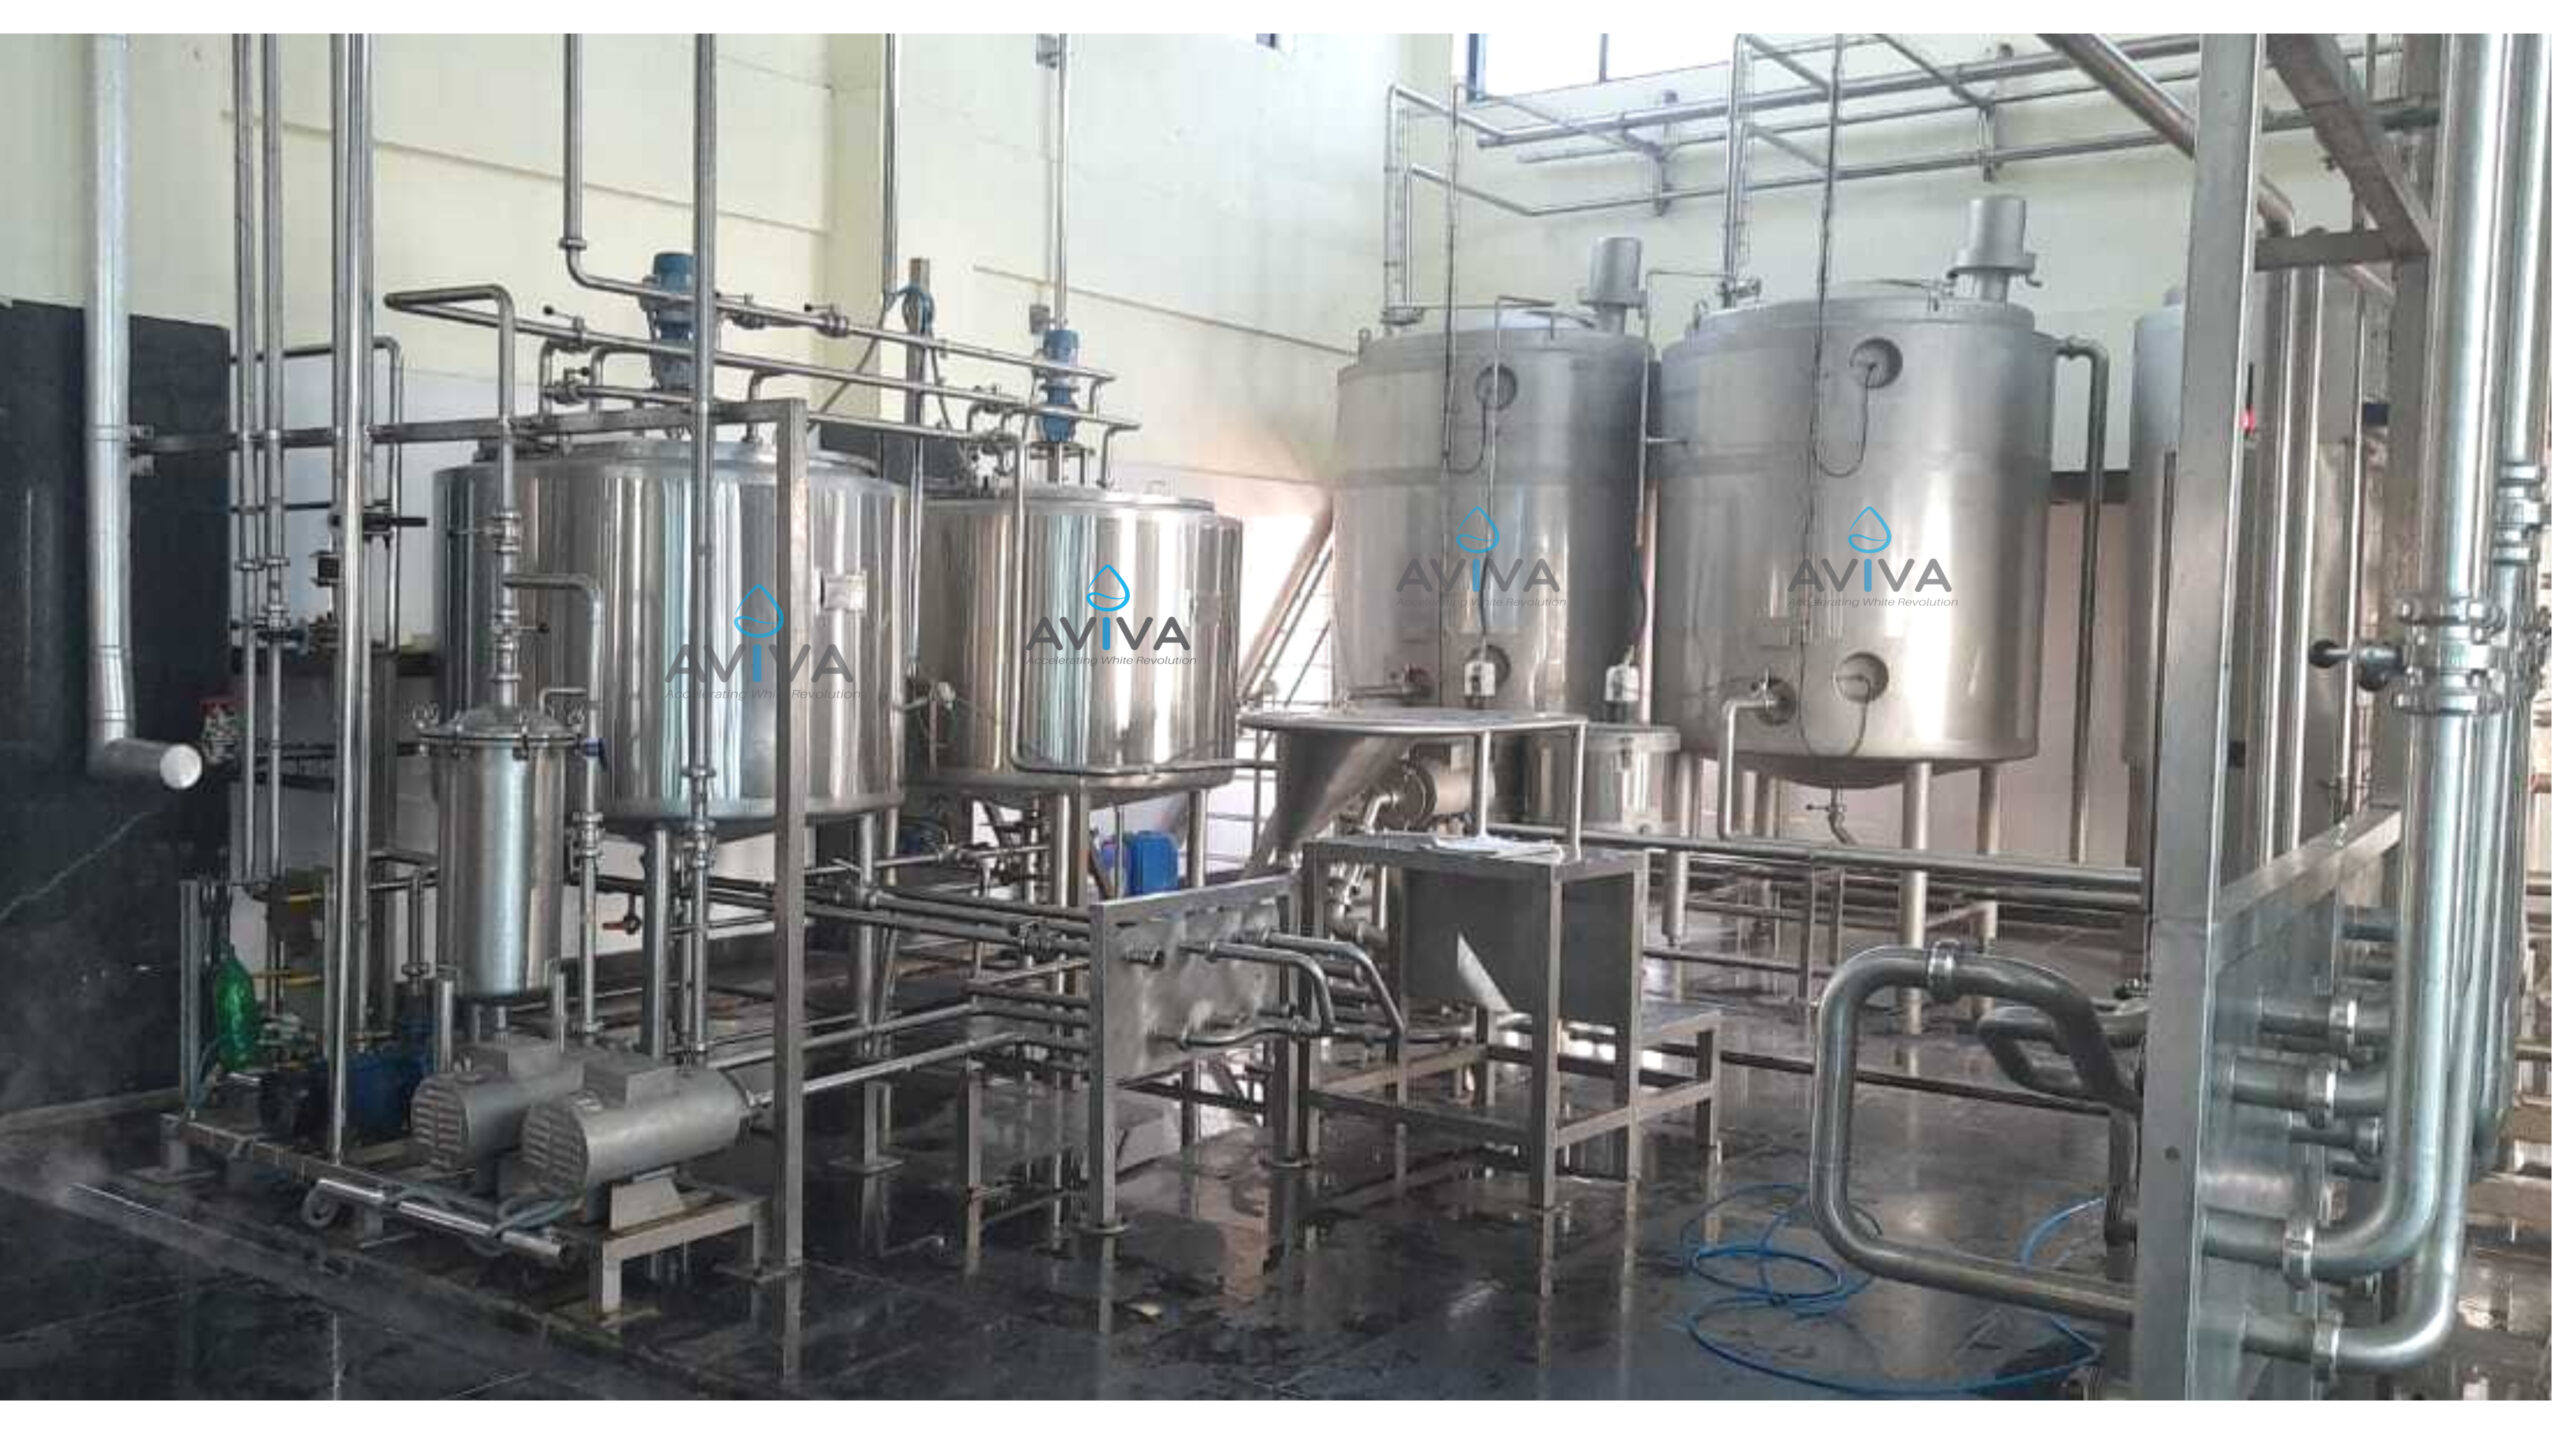
The recondensing section recovers and condenses vapors from evaporation processes, often used in dairy plants to improve energy efficiency and minimize product loss.
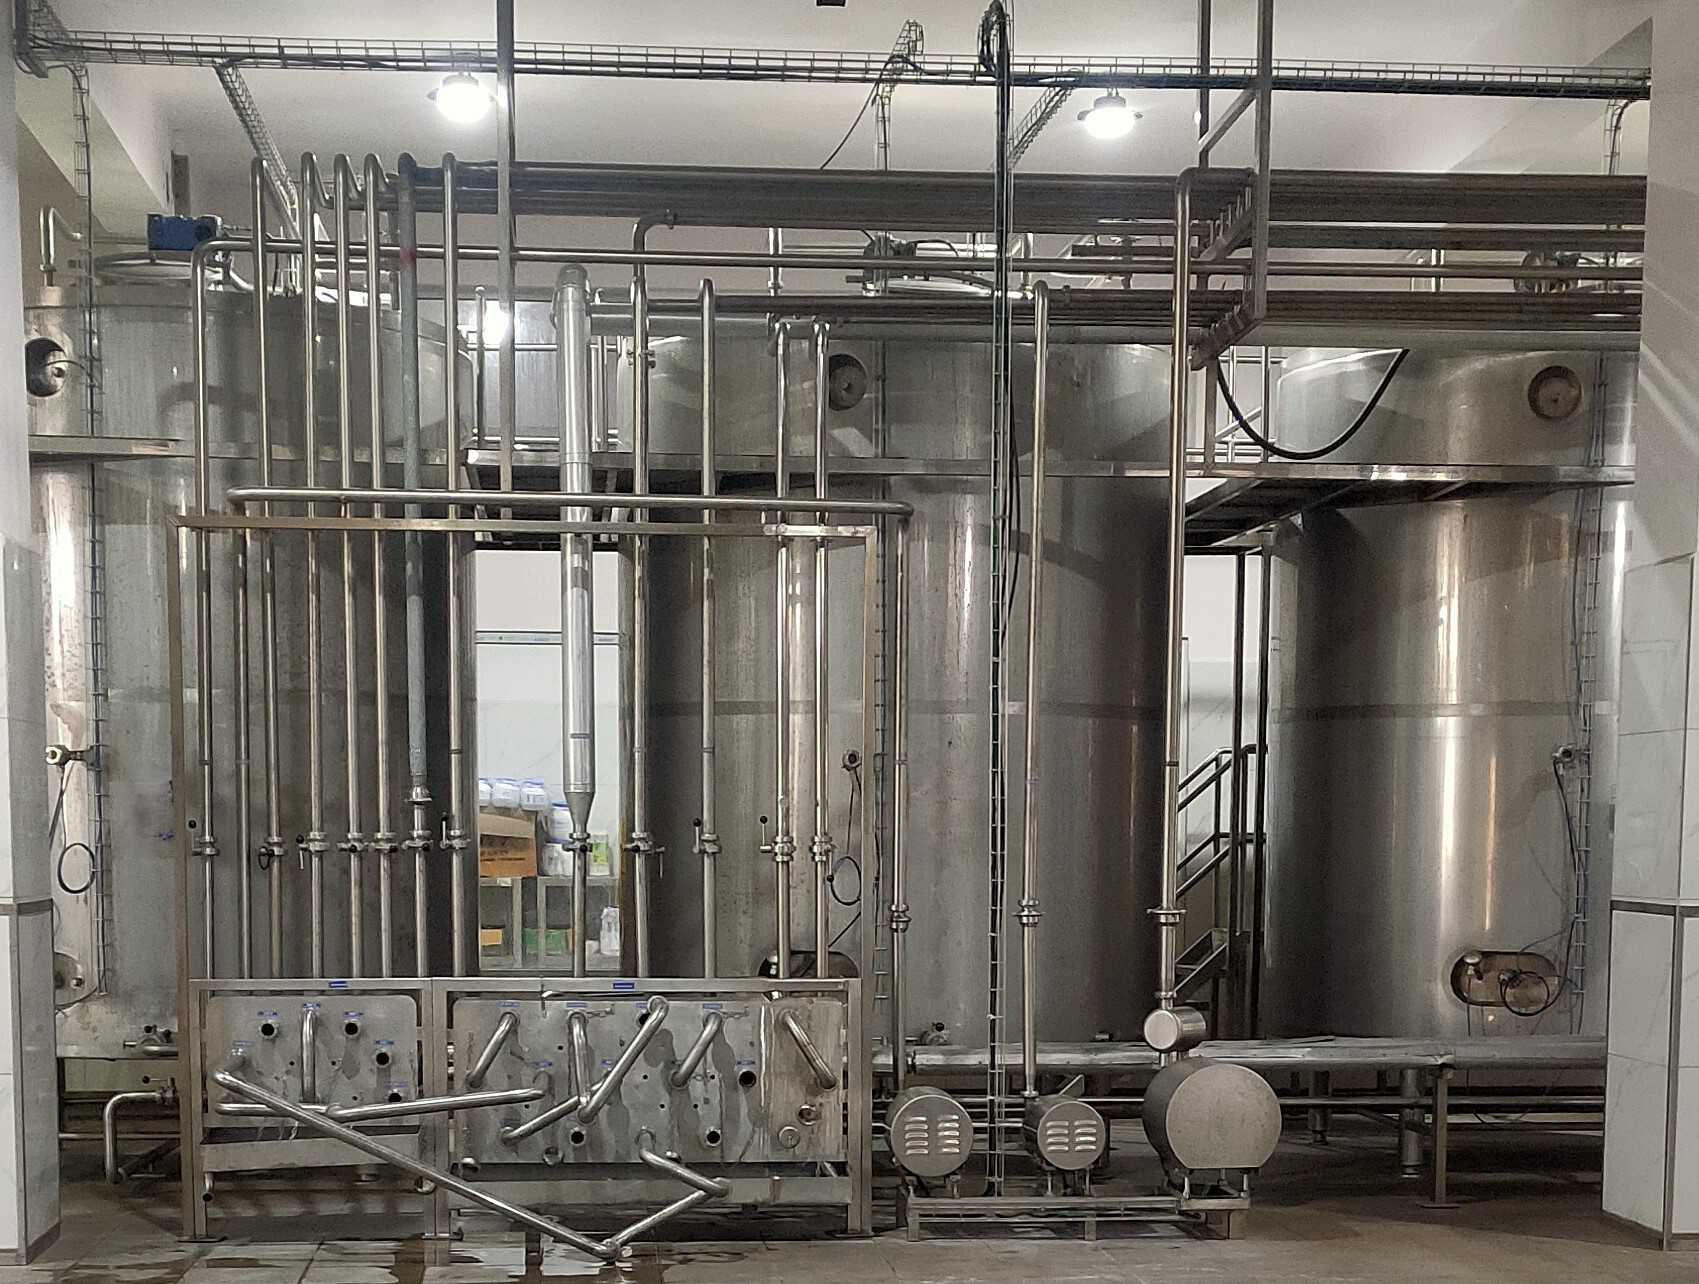
The processed milk storage section holds pasteurized milk in insulated, temperature-controlled tanks to maintain freshness and quality before packaging or further processing.
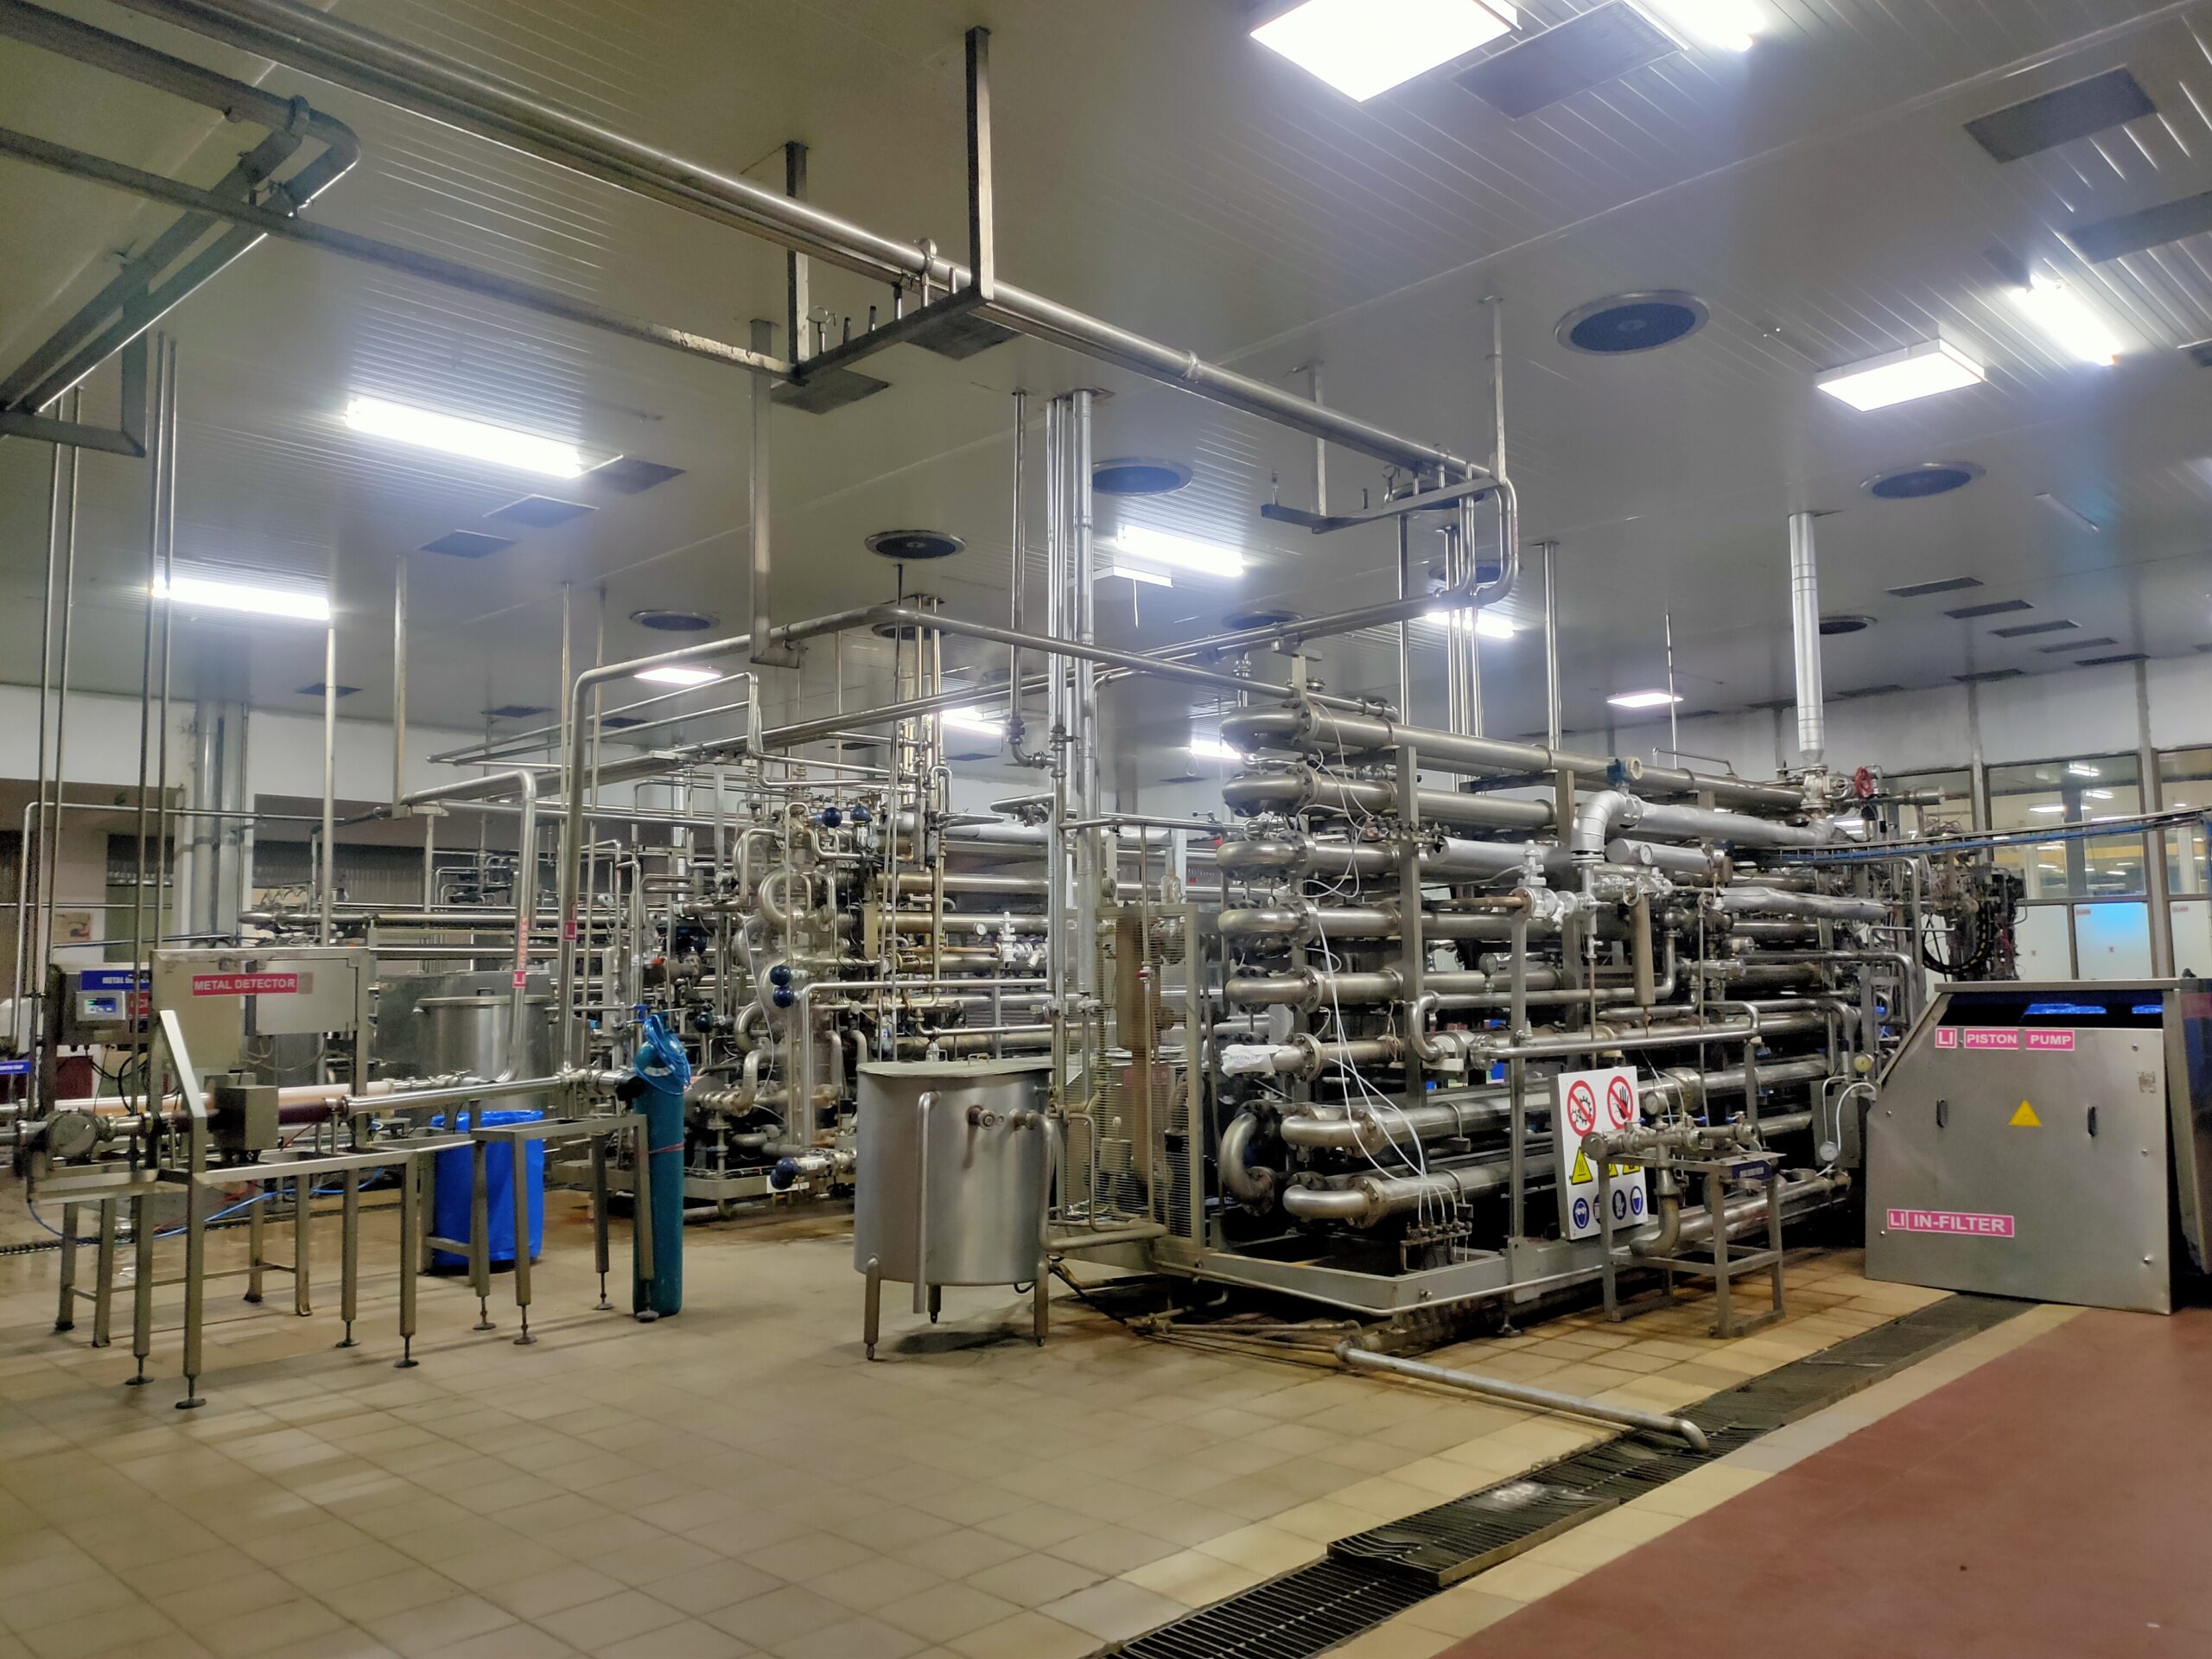
A UHT (Ultra-High Temperature) plant sterilizes milk or liquid products by heating them to 135-150°C for 2-5 seconds, ensuring a long shelf life without refrigeration while preserving nutritional value.
The PCC panel section manages and distributes electrical power to plant equipment, ensuring efficient operation and safety.
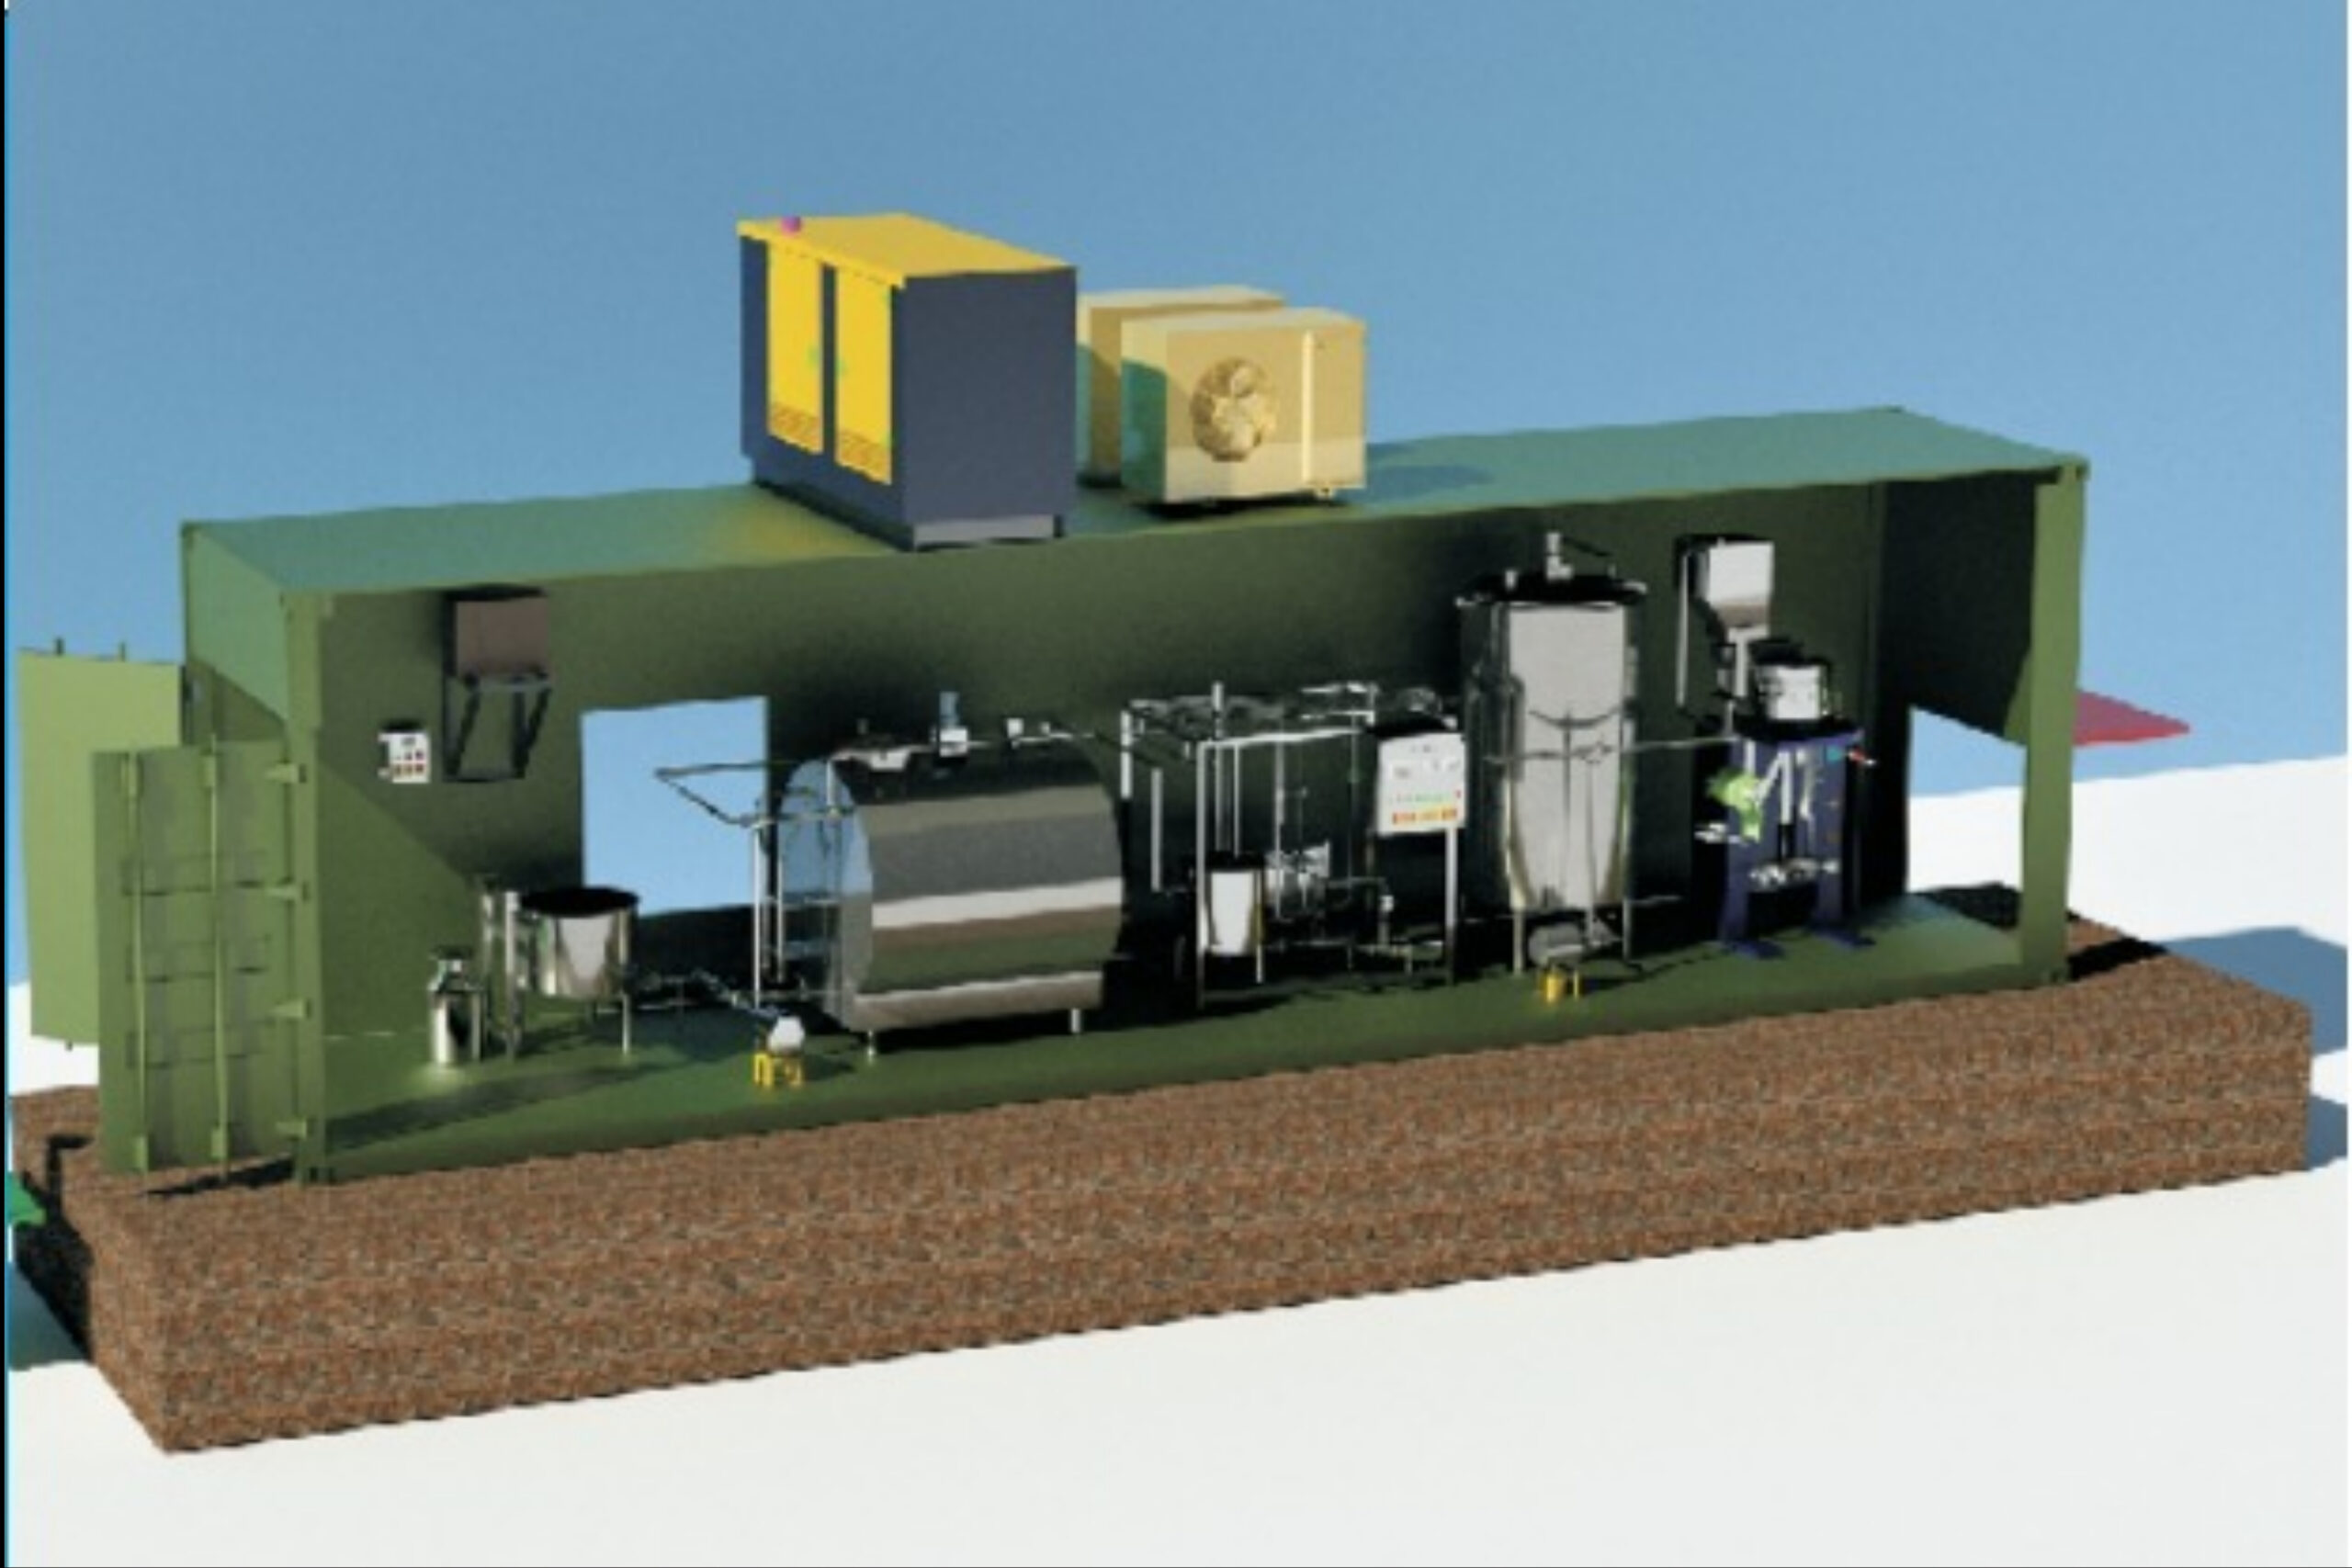
A mini milk processing plant with a capacity of 20 KLPD (kiloliters per day) processes raw milk into various dairy products like pasteurized milk, cream, and butter.
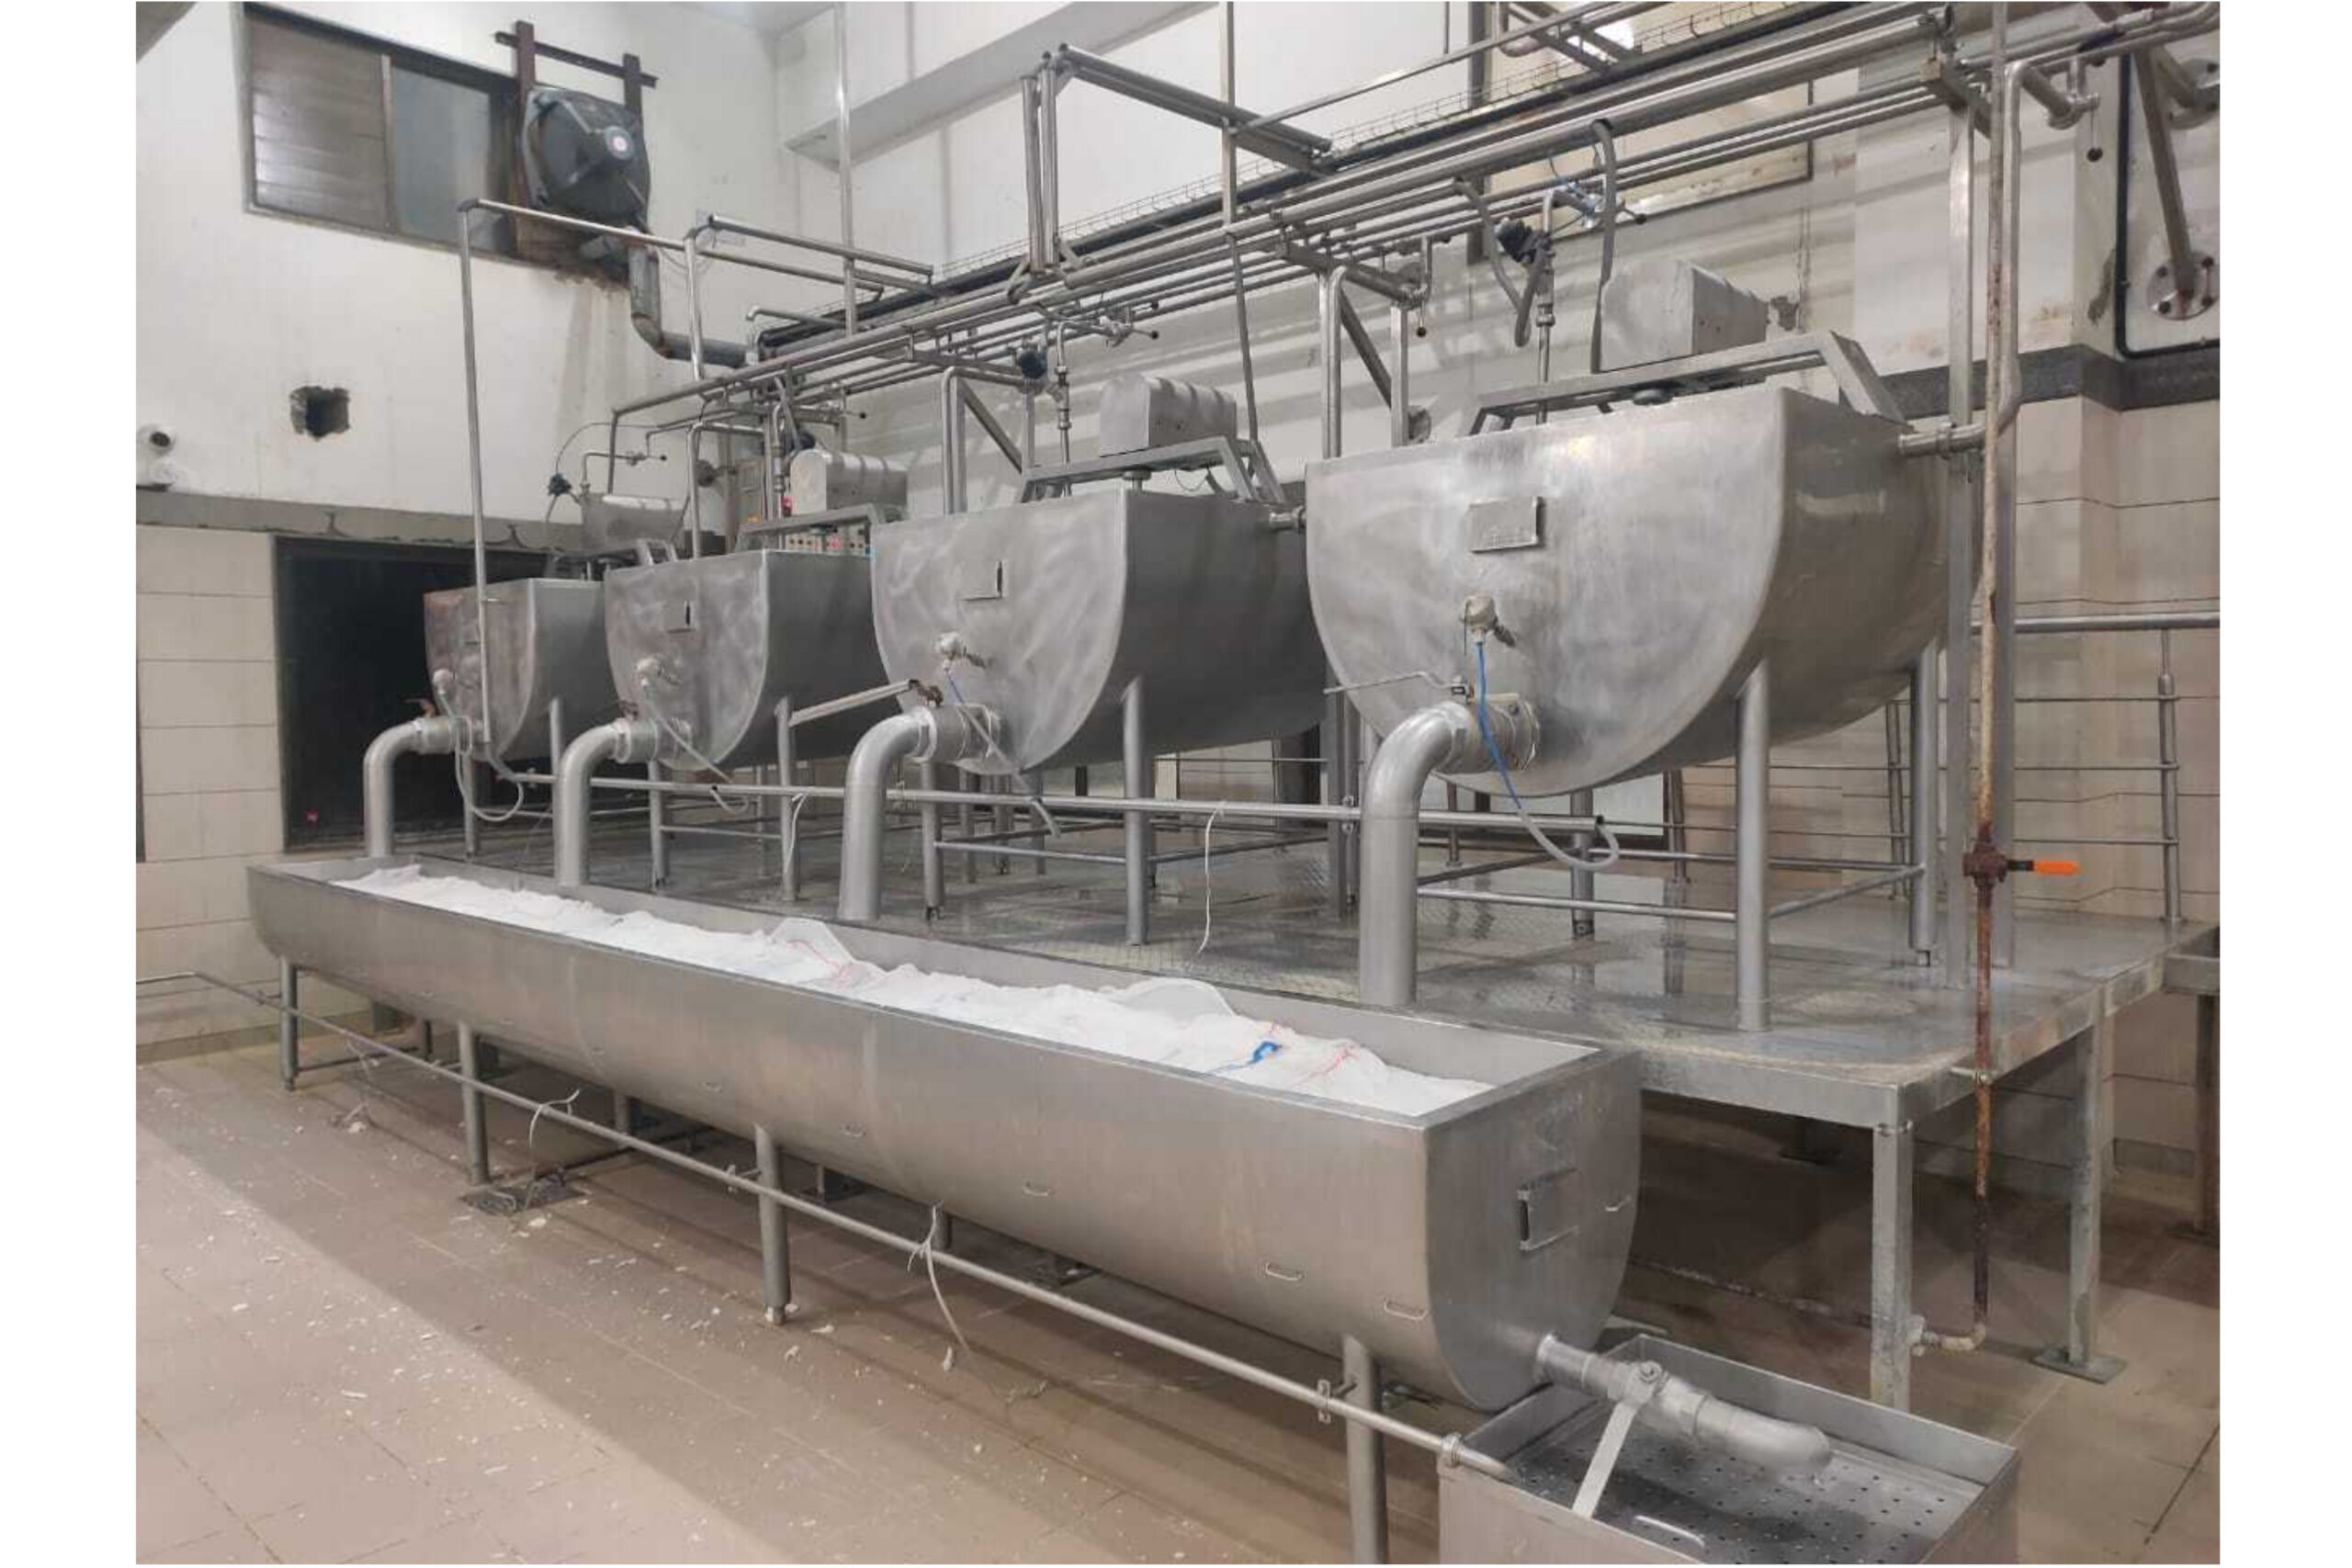
Complete process plant solutions engineered for efficient dairy production, hygiene and reliable industrial performance.
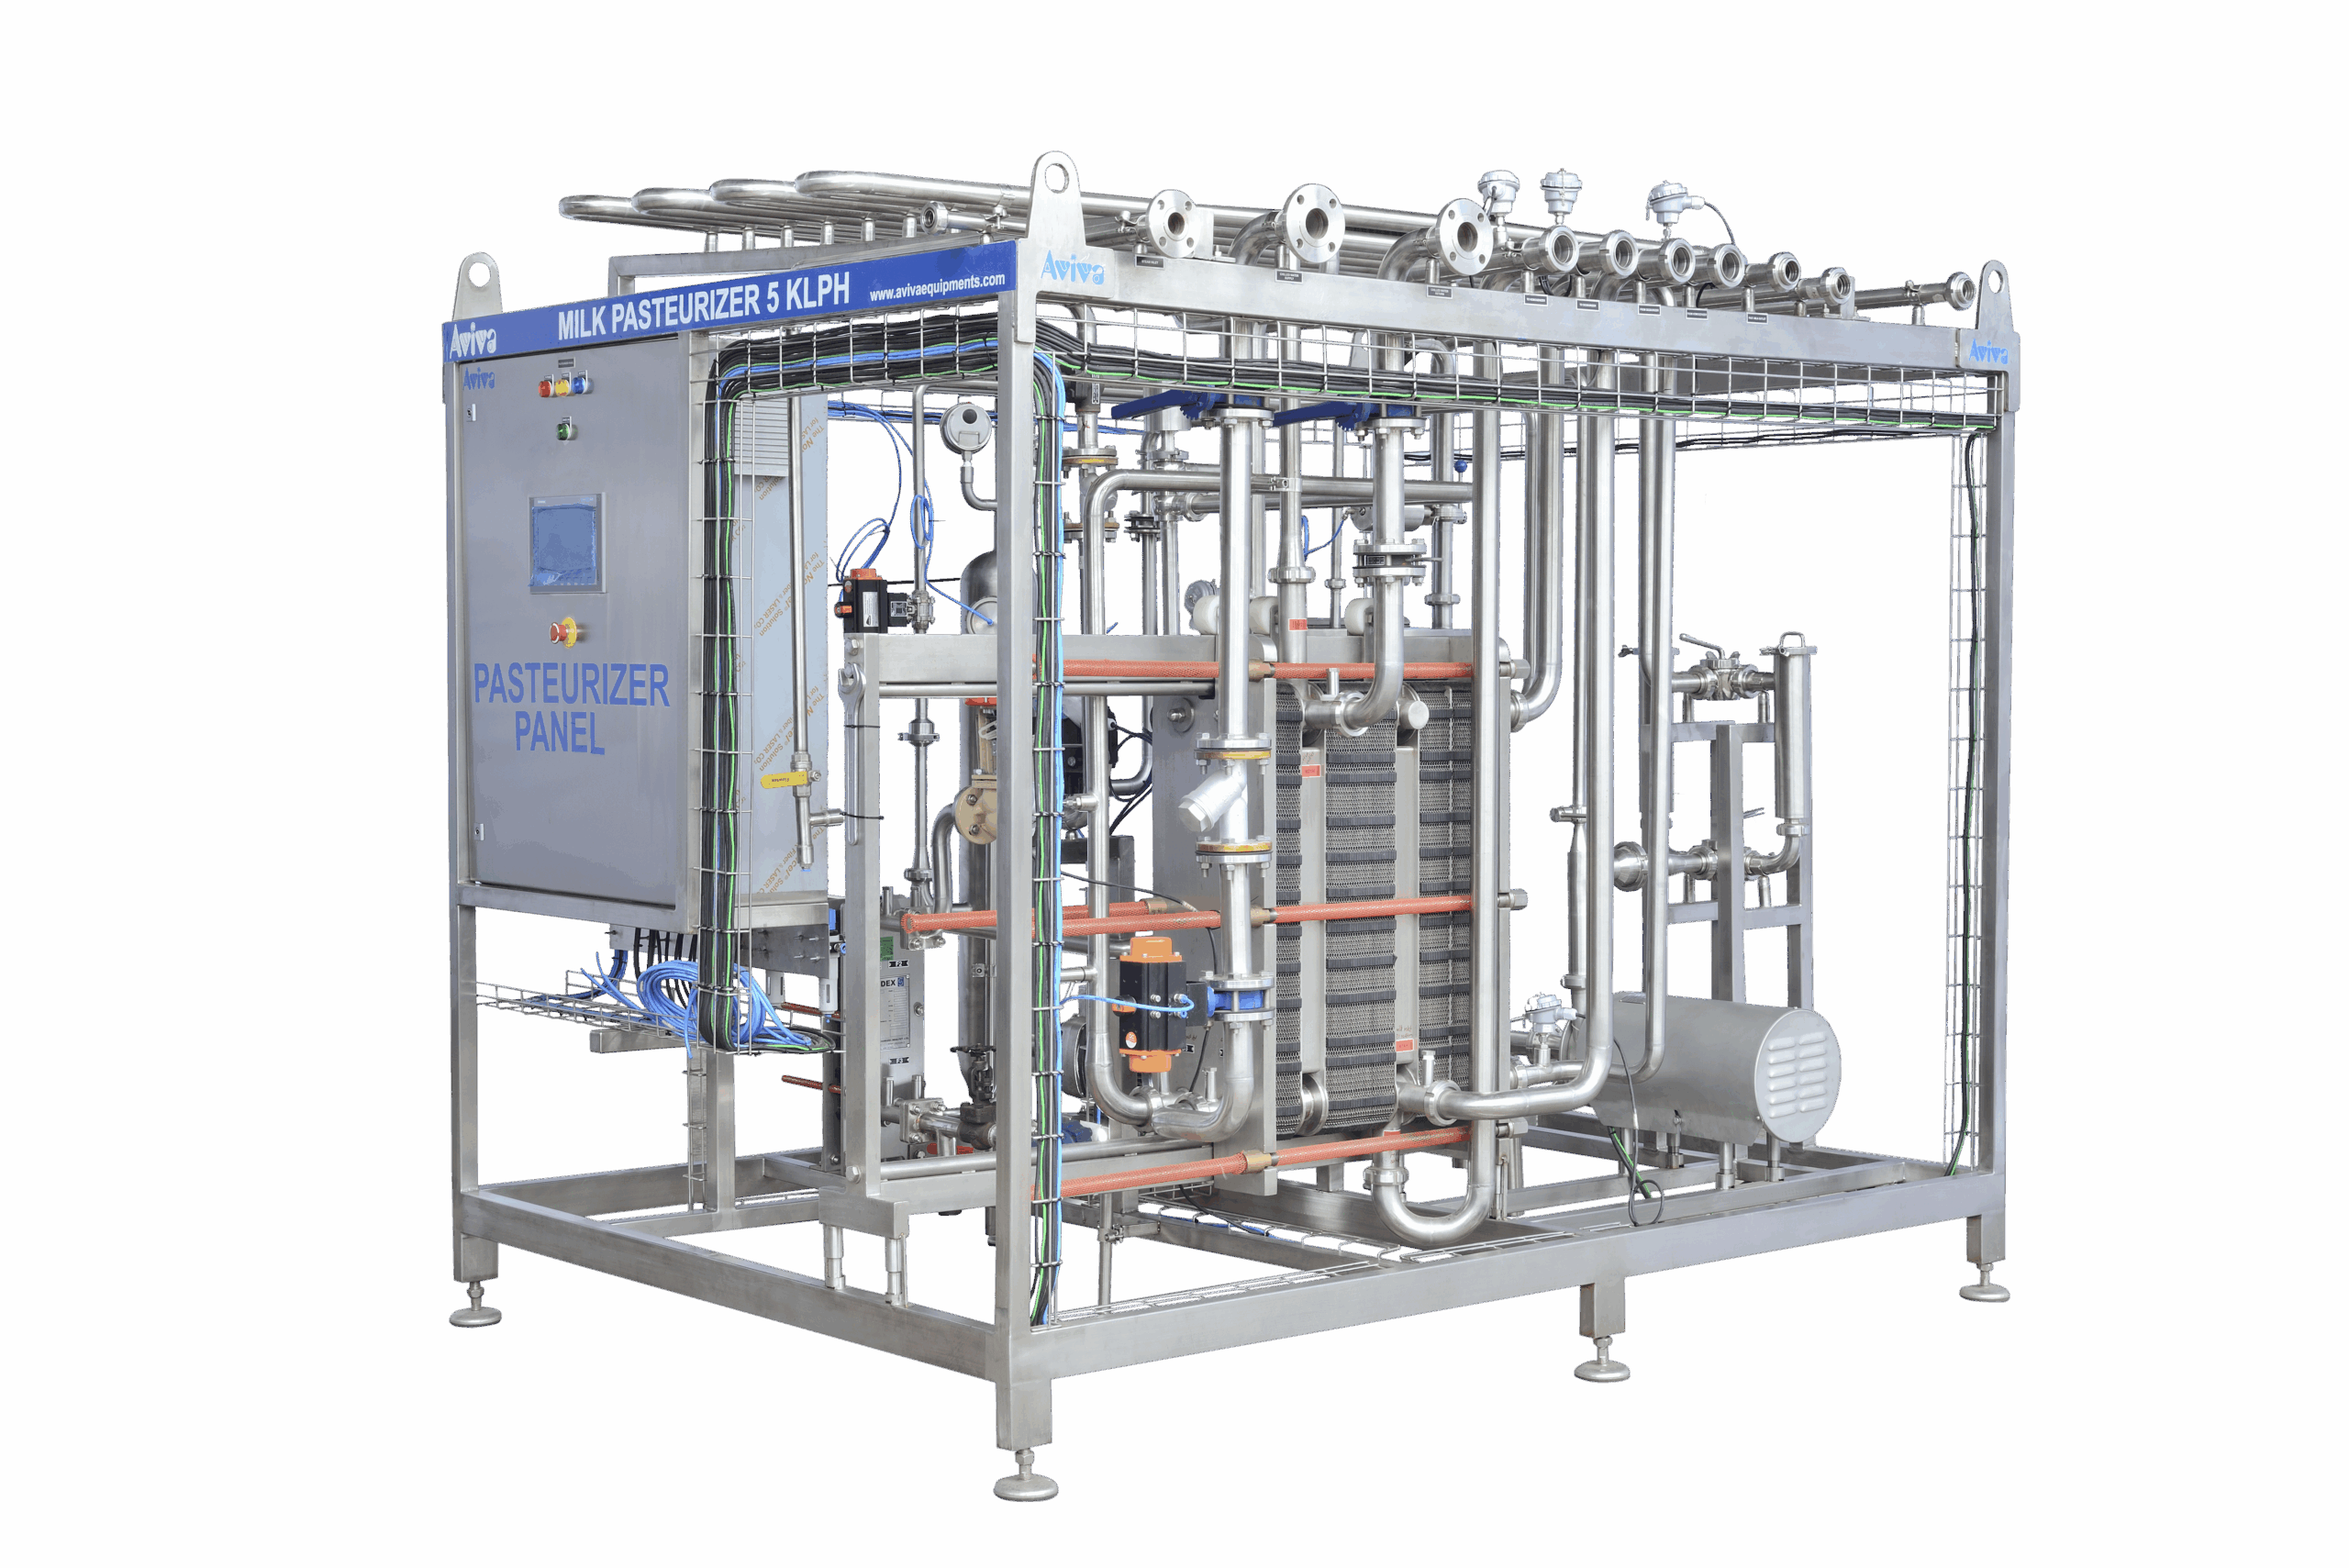
A cream pasteurizer in the dairy industry heats cream to a specific temperature to kill harmful bacteria, ensuring safety and extending shelf life while preserving quality.
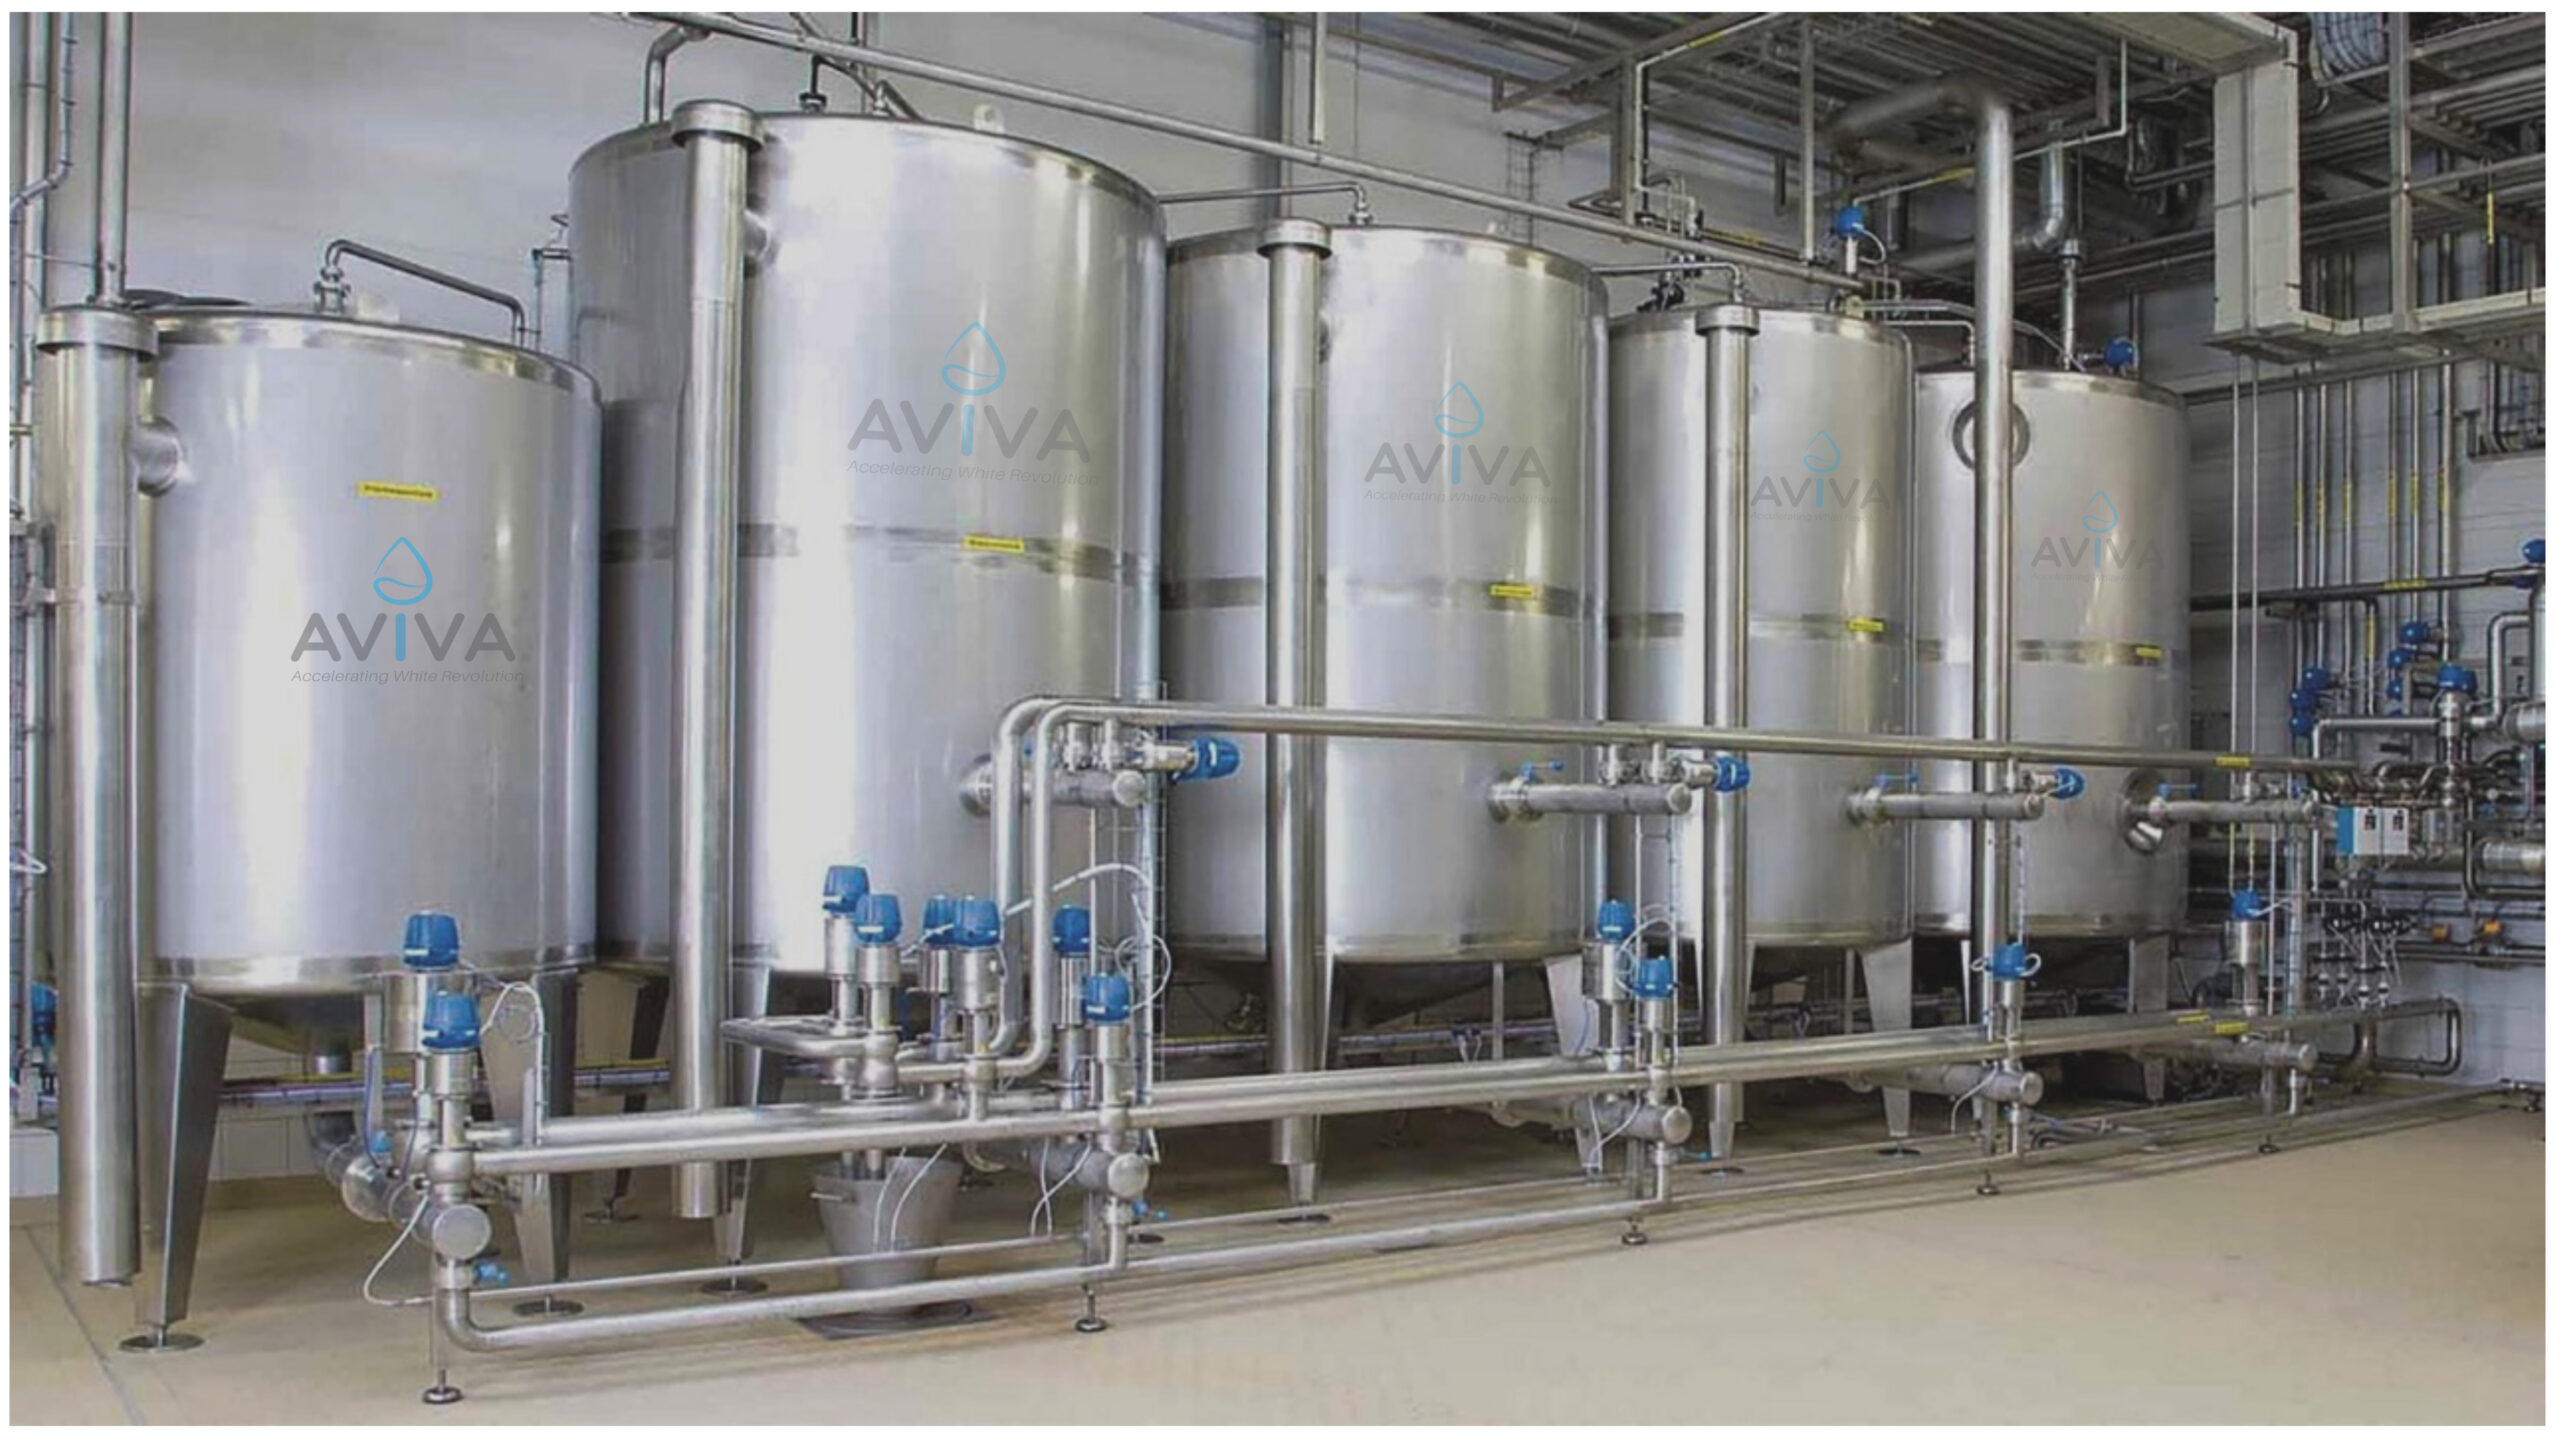
Cleaning of equipment is the most critical job in food processing. Very effective cleaning of the equipment is required for hygienic processing and maintaining product quality.
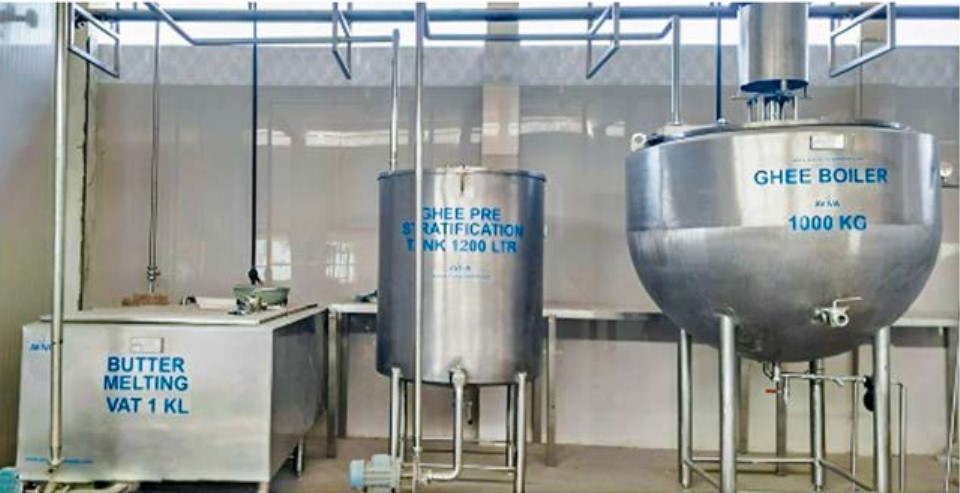
Specialized ghee boilers and plant equipment for clarified butter production with hygienic stainless-steel construction.
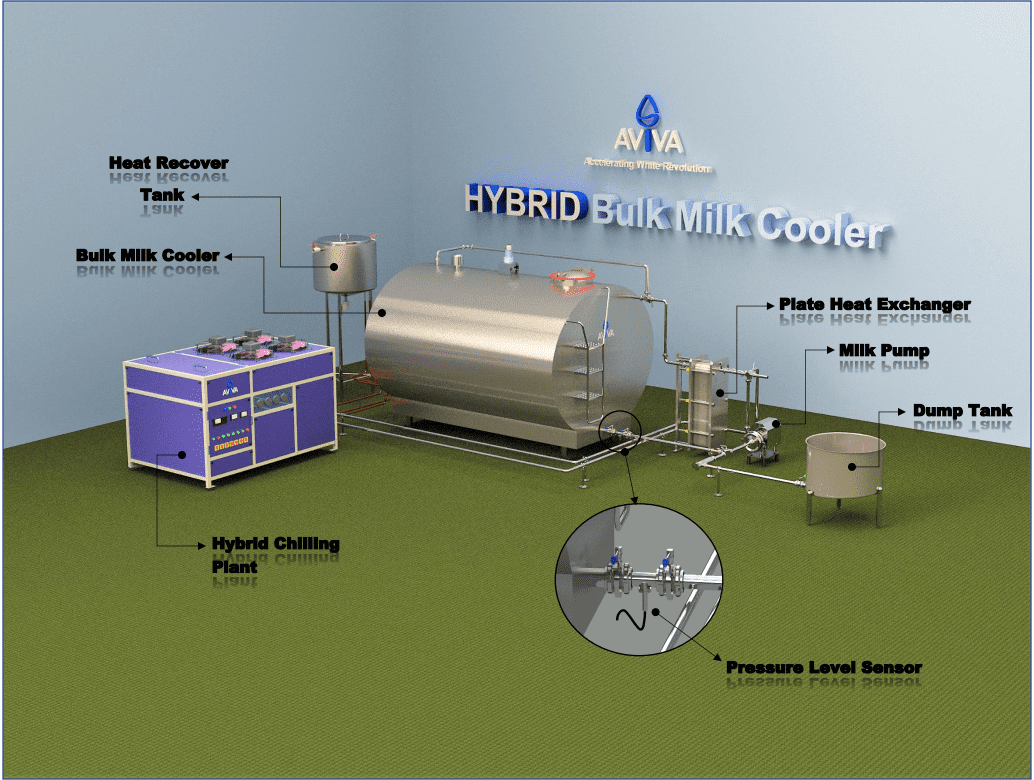
Hybrid bulk milk cooling systems for efficient milk chilling and storage at collection points and dairy plants.
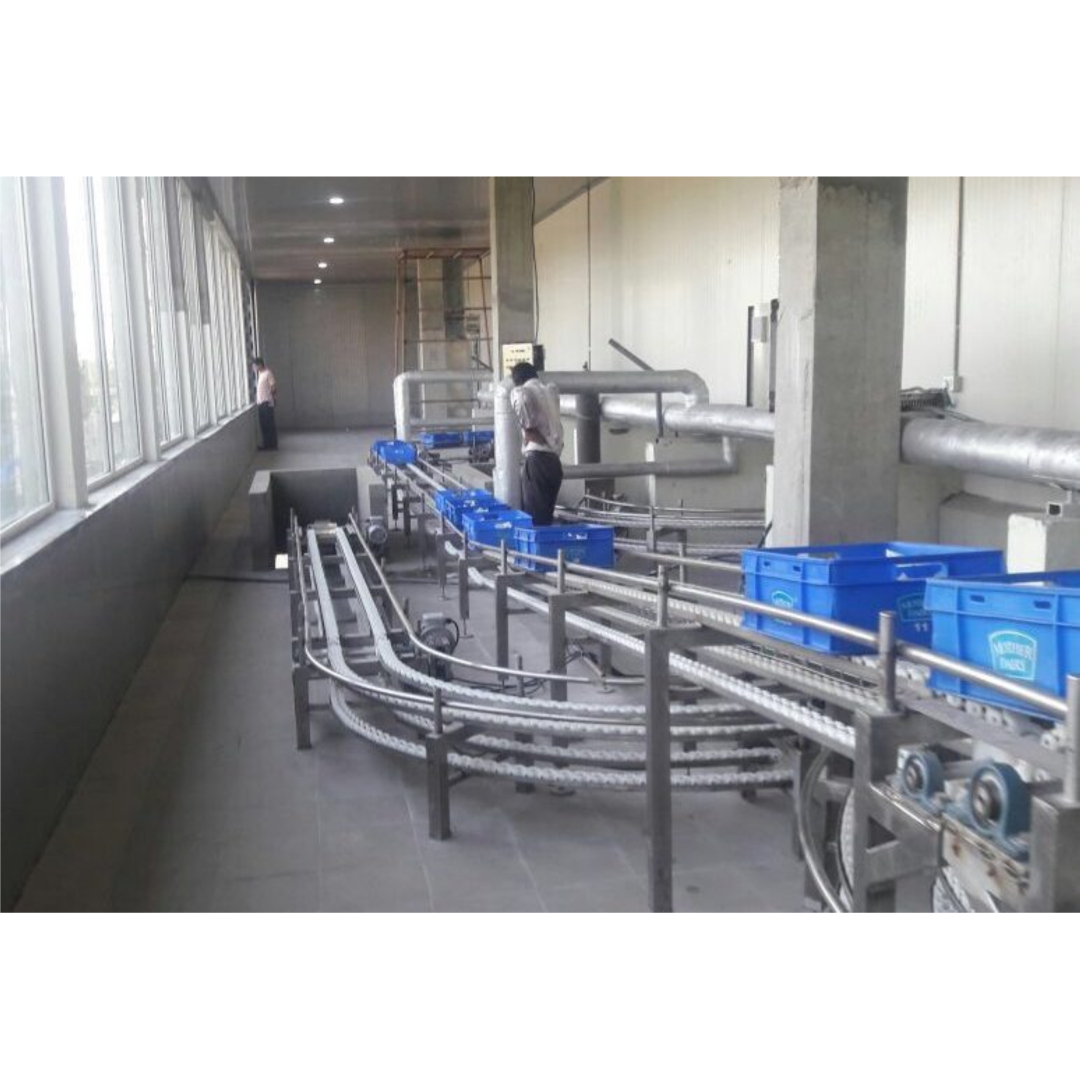
Cold room and blast room solutions for dairy product storage and rapid chilling requirements.
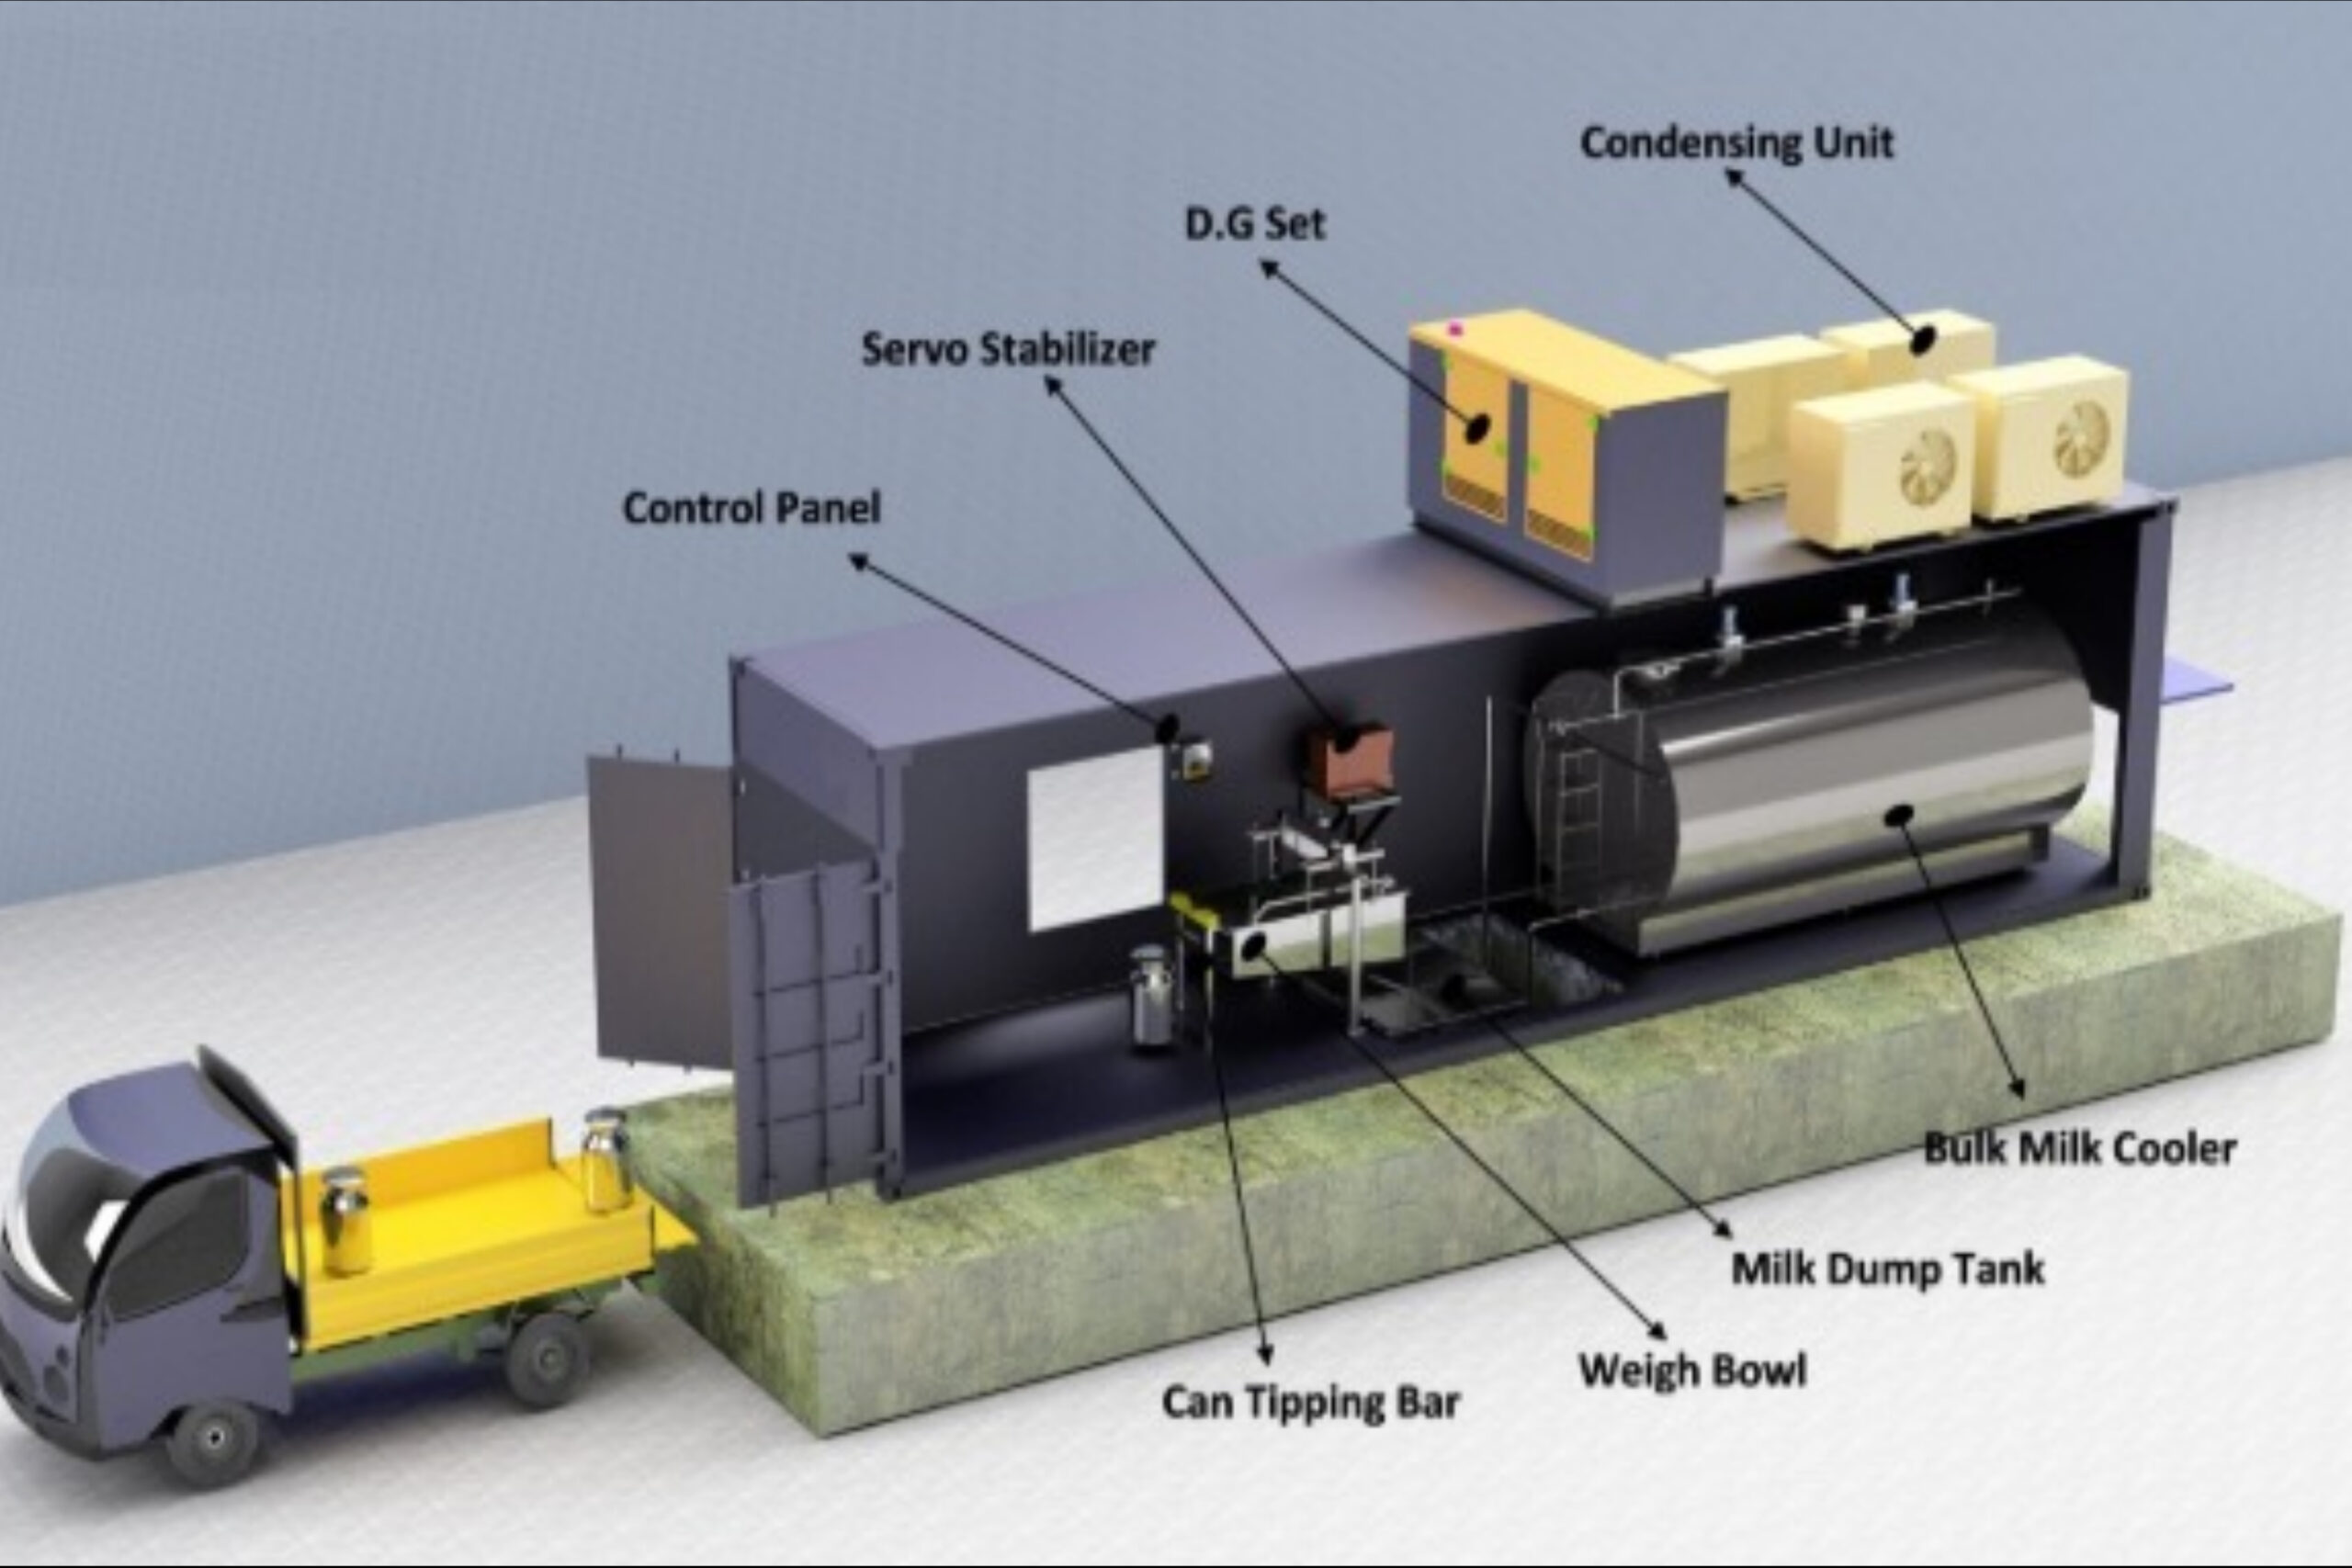
Containerised mini milk chilling plants for flexible, ready-to-deploy milk cooling capacity.